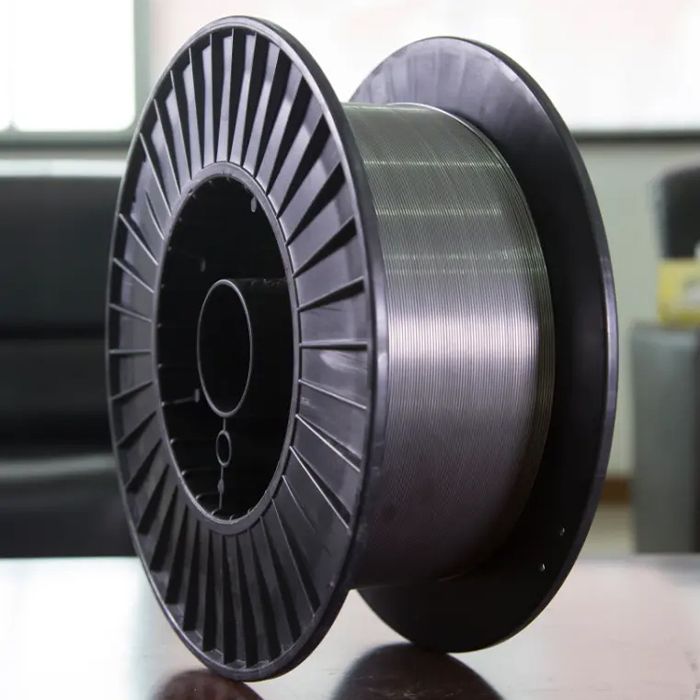
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Features
ENiCrMo3T0-4 Welding Wire used for gas tungsten arc welding (GTAW/TIG)
ENiCrMo3T0-4 Welding Wire used for gas metal arc welding (GMAW/MIG)
ENiCrMo3T0-4 Welding Wire is for dissimilar joints between nickel alloys and stainless steels
ENiCrMo3T0-4 Welding Wire offering excellent high-temperature strength
ENiCrMo3T0-4 Welding Wire offering crack resistance and good low-temperature impact toughnes
Standard: AWS A5.34 ENiCrMo3T0-4 | Chemical Composition % |
| C | Si | Mn | P | S | Cr | Ni | Nb+Ta | Fe | Cu | Mo | Ti | Al | Rest |
Grade ENiCrMo3T0-4 | ≤0.1 | ≤0.5 | ≤0.5 | ≤0.02 | ≤0.015 | 20~23 | ≥58.0 | 3.15~4.15 | ≤5.0 | ≤0.5 | 8~10 | ≤0.40 | ≤0.40 | ≤0.50 |
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Down Load
![]() AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire.pdf
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Specifications
Type | Spool (MIG) |
Specification
( MM ) | 0.8、1.0、1.2、1.6、2.0、2.4、3.2 | Pack | S100/1kg S200/5kg S270,S300/15kg-20kg |
Mechanical Properties | Tensile Strength / MPa | A (%) |
----- |
|
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire video
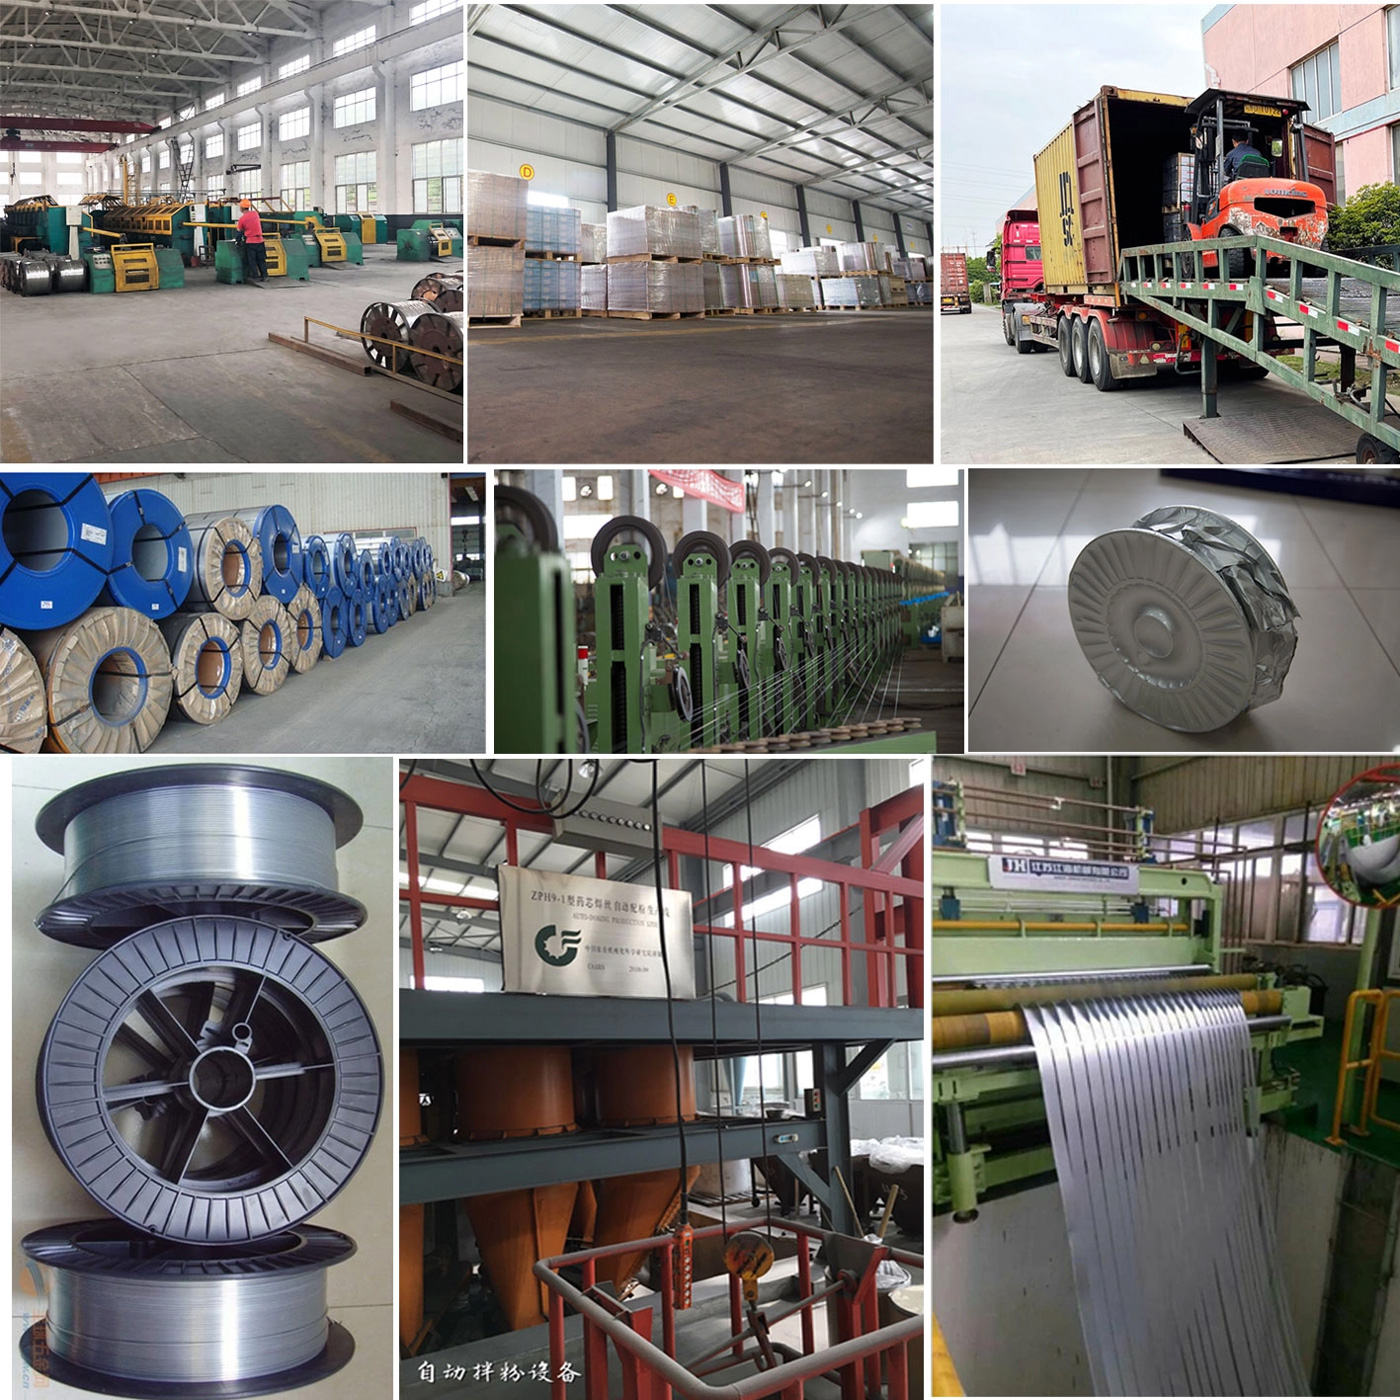
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Factory
![AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire]()
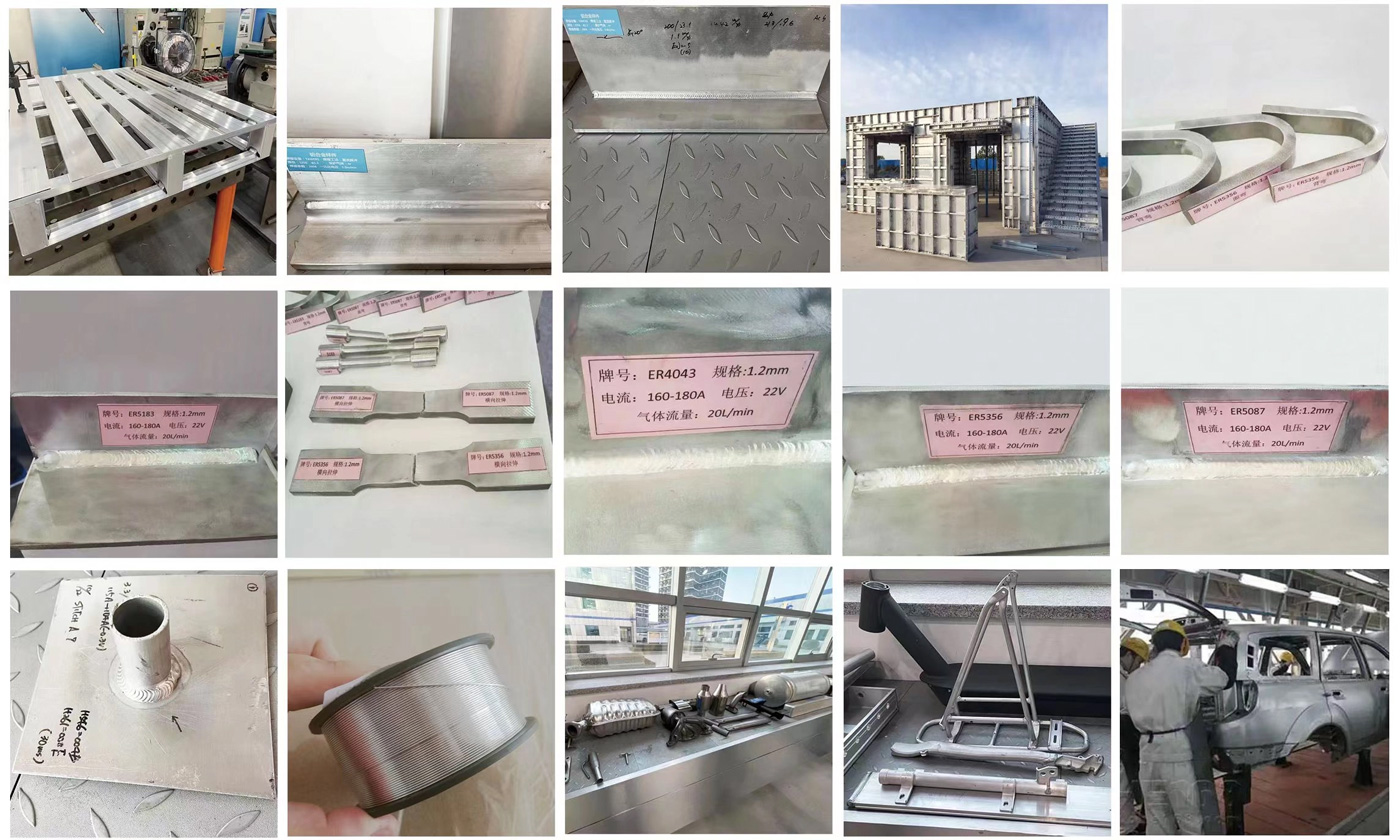
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Application
AWS A5.34 ENiCrMo3T0-4-Nickel alloy self-shielded flux cored wire is the most widely used in the welding of important structures such as shipbuilding.
![AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire]()
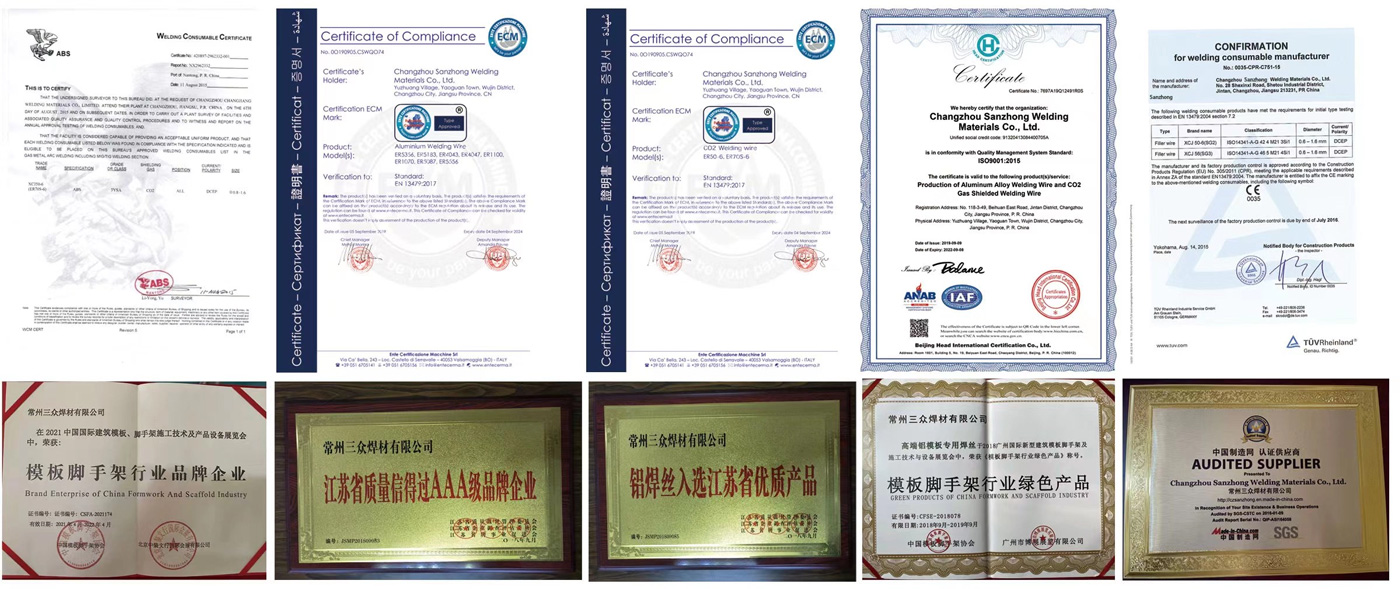
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Certification
![AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire]()
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire WHAT YOU GET
best AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire
Choose Your ENiCrMo3T0-4 Welding Wire Size in mm: 0.8mm / 0.9mm / 1.0mm / 1.2mm/ 1.6mm
Choose Your ENiCrMo3T0-4 Welding Wire Size in inch: 0.030 / 0.035 / 0.040 / 0.045/ 0.063/ 0.079 / 3/16
Choose Your ENiCrMo3T0-4 Welding Wire Spool Weight(Package): 5kg / 15kg / 20kg
Choose Your ENiCrMo3T0-4 Welding Wire Size: 1.2mm/ 1.6mm/ 2.0mm
Choose Your ENiCrMo3T0-4 Welding Wire Package: 2kg / 5kg / 10kg / 1LB / 2LB / 4.5LB / 15.5LB / 20LB
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire knowledge
Best AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Requirements
The requirements for ERNiCrMo3T0-4 welding wire are defined by the AWS A5.34 standard for solid wire and AWS A5.11 for covered electrodes. Meeting these standards ensures the wire's chemical composition, mechanical properties, and conformance for critical applications.
Typical values from manufacturers often show lower impurities, e.g., C: 0.02%, Mn: 0.3%, Fe: 4.5%, ensuring high-quality deposits .
Base Materials: The wire is designed for welding Inconel 625, 800/800H, 825 alloys, super duplex stainless steels .
Electrode Drying (for Stick Electrodes): Covered electrodes (AWS A5.11) typically require baking at 350°C for 1 hour before use .
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Identification
AWS / SFA A5.34: ERNiCrMo3T0-4 is the standard classification for solid wire used in MIG/TIG welding .
EN ISO 18274: The equivalent international classification is S Ni 6625 (or NiCr22Mo9Nb) .
Covered Electrode: For stick electrodes (SMAW), the AWS standard is A5.11 ENiCrMo-3 .
Flux-Cored Wire: For flux-cored wires, the classification is AWS A5.34 ENiCrMo3T1-4 .
AWS A5.34 ENiCrMo3T0-4-Nickel alloy self-shielded flux cored wire, all position, Inconel 625 type
Markings on the Wire: Some manufacturers physically stamp or punch the AWS code on each wire (e.g., "ERNiCrMo-3"), providing direct positive identification .
TIG Rods: Typically cut to lengths (e.g., 1000 mm) and sold in plastic containers or polythene bags of weights like 5 kg .
MIG Wire: Supplied on spools or in metallic rings, often in 25 kg packages .
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Packaging
ENiCrMo3T0-4 welding wire is available in packaging specifically designed to protect the material and suit different welding processes. The main forms are spooled wire for MIG (GMAW) welding and cut-length rods for TIG (GTAW) welding.
(1) Spooled WireMIG/GMAW welding Typically 12.5 kg (approx. 27.6 lbs) or 15 kg per spool
(2) Cut-Length RodsTIG/GTAW welding Usually packaged in boxes of 5 kg
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire WARNING
gas shielded flux cored wire,Before use, read and understand the manufacturer's instructions, Material Safety Data Sheets (MSDSs), and your employer's safety practices.
stainless steel flux core wire types have too many kinds ,Keep your head out of the fumes.Use enough ventilation, exhaust at the arc, or both, to keep fumes and gases away from your breathing zone and the general area.Wear correct eye, ear, and body protection.
flux wire welder,Do not touch live electrical parts.See American National Standard, ANSI 249.1, Safety in Welding.
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire FAQ
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire 10 famous brand are which factory?
1:sanzhong, 2:giant, 3:bohler, 4:rural king, 5:lincoln, 6:hyundai, 7:blue demon, 8:esab, 9:Oxford, 10:golden bridge
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire supplier and factories or wholesale locates in such countries like?
China,America,Brazil,England,Russia,Poland,India,Pakistan,NewZealand,Korea,Australia,Dubai,Turkey,Indonesia,UAE.
AWS A5.34 ENiCrMo3T0-4 VS ENiCrMo3T1-4?
ENiCrMo3T0-4 and ENiCrMo3T1-4 are both AWS A5.34 nickel alloy flux cored welding wires with identical deposited metal chemical composition (Inconel 625 type). The main difference lies in shielding system: ENiCrMo3T0-4 is self-shielded and works without external shielding gas, ideal for field on-site repair. ENiCrMo3T1-4 is gas-shielded flux cored wire using CO₂ or Ar‑CO₂ mixed gas; it delivers superior weld appearance and excellent cryogenic impact property, widely used for LNG tanks and pressure vessel fabrication. Both wires are classified for all-position welding (-4 suffix), suitable for dissimilar welding between nickel alloy, stainless steel and carbon steel.
AWS A5.34 ENiCrMo3T0-4 VS ENiCrMo-3?
ENiCrMo3T0-4 (AWS A5.34) self-shielded flux cored wire and ERNiCrMo-3 (AWS A5.14) solid nickel alloy wire generate Inconel 625 weld deposit with similar chemical composition and corrosion resistance. ENiCrMo3T0-4 works without external shielding gas and is suitable for field all-position repair welding, while ERNiCrMo-3 solid wire requires pure argon shielding, delivering cleaner weld bead and excellent low-temperature toughness for indoor precision fabrication and critical component welding.
AWS A5.34 ENiCrMo3T0-4 VS AWS A5.34 ENiCrCoMo T1-4?
ENiCrMo3T0-4 and ENiCrCoMoT1-4 are both nickel alloy flux cored wires classified under AWS A5.34 for all-position welding. ENiCrMo3T0-4 is self-shielded without external shielding gas. It contains niobium and delivers outstanding resistance to chloride, pitting and crevice corrosion, suitable for on-site dissimilar metal repair in chemical and offshore environments. ENiCrCoMoT1-4 is gas-shielded, with cobalt added to greatly improve high-temperature oxidation and creep resistance, ideal for high-temperature components such as gas turbine and furnace overlay. ENiCrCoMoT1-4 needs shielding gas during welding and costs higher due to cobalt content.
AWS A5.34 ENiCrMo3T0-4 VS ENiCrCoMo T0-4Inconel 617?
ENiCrMo3T0-4 and ENiCrCoMoT0-4 are both AWS A5.34 self-shielded nickel alloy flux cored wires for all-position welding without external shielding gas. ENiCrMo3T0-4 is Inconel 625 type with niobium addition, designed for field dissimilar metal welding and components exposed to chloride, pitting and crevice corrosion in chemical and offshore environments. ENiCrCoMoT0-4 is Inconel 617 type containing cobalt, aluminium and titanium, which provides superior high-temperature creep and oxidation resistance, ideal for furnace and gas turbine component repair. Both wires are self-shielded for on-site welding, but not interchangeable due to different alloy design for corrosion vs high-temperature creep service.
AWS A5.34 ENiCrMo3T0-4 VS AWS A5.34 ENiCrCoMo T0-4?
ENiCrMo3T0-4 and ENiCrCoMoT0-4 are both AWS A5.34 self-shielded nickel alloy flux cored wires for all-position welding without external shielding gas. ENiCrMo3T0-4 is Inconel 625 type with niobium addition, designed for field dissimilar metal welding and components exposed to chloride, pitting and crevice corrosion in chemical and offshore environments. ENiCrCoMoT0-4 is Inconel 617 type containing cobalt, aluminium and titanium, which delivers superior high-temperature creep and oxidation resistance, ideal for furnace and gas turbine component repair. Both wires are self-shielded for on-site welding, but they are not interchangeable due to different alloy designs for corrosion and high-temperature service respectively.
AWS A5.34 ENiCrMo3T0-4 under FCAW-G and FCAW-S?
ENiCrMo3T0-4 is classified under AWS A5.34 for FCAW-S (self-shielded flux cored arc welding) and cannot be used for FCAW-G. Its matching gas-shielded grade is ENiCrMo3T1-4 for FCAW-G. Both wires produce identical Inconel 625-type weld deposit for all-position welding. ENiCrMo3T0-4 relies only on internal flux for arc protection, ideal for field on-site repair where shielding gas is unavailable. ENiCrMo3T1-4 needs external shielding gas, delivering cleaner weld bead and better low-temperature toughness for indoor precision fabrication.
All wire under and according to the AWS A5.34 standard?
AWS A5.34 covers nickel alloy flux cored wires including ENiCrMo3, ENiCrCoMo, ENiCrFe3, ENiMo10, ENiMo13 and ENiCrMo4, where T0 denotes self-shielded
type, T1 gas-shielded type and -4 all-position welding.
ENiCrMo3T0-4 — Self-shielded, Inconel 625 type, all position
ENiCrMo3T1-4 — Gas-shielded, Inconel 625 type, all position
ENiCrCoMoT0-4 — Self-shielded, Inconel 617 type, all position
ENiCrCoMoT1-4 — Gas-shielded, Inconel 617 type, all position
ENiCrFe3T0-4 — Self-shielded, Inconel 82 type
ENiCrFe3T1-4 — Gas-shielded, Inconel 82 type
ENiMo10T1-4 — Gas-shielded, Hastelloy B2 type
ENiMo13T1-4 — Gas-shielded, Hastelloy B3 type
ENiCrMo4T1-4 — Gas-shielded, Hastelloy C276 type
Metal cored grades adopt AWS A5.14 alloy designation: ERNiCrMo-3, ERNiCrCoMo-1, ERNiCrFe-3, ERNiMo-10, ERNiMo-13, ERNiCrMo-4
AWS A5.34 covers nickel alloy flux cored (FCAW) and metal cored welding electrodes. The main flux-cored classifications include ENiCrMo3 (625),
ENiCrCoMo (617), ENiCrFe3 (82), ENiMo10, ENiMo13 and ENiCrMo4. The suffix T0 stands for self-shielded, T1 for gas-shielded; -4 means all-position welding.
Metal cored electrodes follow AWS A5.14 alloy names.
Bullet points (product page simple list)
ENiCrMo3T0-4 / ENiCrMo3T1-4 (Inconel 625)
ENiCrCoMoT0-4 / ENiCrCoMoT1-4 (Inconel 617)
ENiCrFe3T0-4 / ENiCrFe3T1-4 (Inconel 82)
ENiMo10T1-4, ENiMo13T1-4 (Hastelloy B series)
ENiCrMo4T1-4 (Hastelloy C276)
AWS A 5.34 ENiCrMo3T0-4 Nickel alloy self-shielded flux cored Welding Wire Use
Welding Matching and Similar Alloys: It is the standard choice for welding nickel-chromium-molybdenum alloys, most notably Inconel® 625, as well as Incoloy® 825, Alloy 20, and other similar high-alloy materials.
Dissimilar Metal Welding: A key use is joining nickel alloys to other metals, such as stainless steels, low-alloy steels, and carbon steels. The filler metal's composition helps manage the different thermal and metallurgical properties of these dissimilar materials.
Specialty Steel Welding: It is frequently used to weld 9% Nickel steels, which are vital in cryogenic (very low-
temperature) applications like LNG storage tanks.
Surfacing and Cladding: The alloy is extensively used to deposit a corrosion-resistant layer onto steel components through weld cladding. This is common in critical industries to protect the underlying metal from harsh environments.
Oil and Gas: Used for welding pipe internals, valves, and other components that must resist pitting and stress corrosion cracking in sour gas (H₂S) and seawater environments.
Chemical Processing and Pollution Control: Its outstanding resistance to a wide range of corrosive chemicals makes it suitable for reactors, piping, and scrubbers.
Power Generation and Aerospace: Used for components that require high strength and oxidation resistance at elevated temperatures (serviceable up to over 1000°C in some cases), including furnace equipment and jet engine parts.
AWS A5.34 ENiCrMo3T0-4 self-shielded nickel alloy flux cored welding wire is used for all-position field welding and corrosion-resistant overlay. It welds Inconel 625 itself, dissimilar joints between nickel alloys, stainless steel, carbon steel and low alloy steel. It is widely applied for offshore equipment, chemical vessels, flue gas desulfurization systems, on-site repair of process piping and components requiring resistance to chloride pitting and crevice corrosion. No external shielding gas is required for outdoor or remote site welding.