AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Features
EFeMn‑A: Hadfield manganese austenitic surfacing electrode, work-hardening, heavy impact resistance
EFeCr‑A: Medium chromium iron hardfacing electrode, balanced abrasion & impact
ECrC‑A: High chromium carbide surfacing electrode, low-stress abrasive wear resistance
ECoCr‑A (Stellite 6): Cobalt base surfacing stick electrode, cavitation & corrosion resistance
ECoCr‑B, ECoCr‑C: Stellite grades for higher hardness or heavy impact
ENiCr-C: Nickel base surfacing stick electrode, anti-galling, corrosion & wear resistant
Standard AWS A5.13 AWS A5.21 | Chemical Composition % |
| C | Cr | Mn | Si | W | Ni | Fe | Co | Other | Hardness (HRC) |
ERFeCr‑A1 | 1.5–3.5 | 8–14 | 0.5–1.5 | ≤2.0 | --- | ≤2 | Bal | --- | --- | 45-52 |
ERFeCr‑A5 | 3.5–6.0 | 24–32 | 0.5–1.5 | ≤2.0 | --- | ≤4 | Bal | --- | Mo≤4 | 58-64 |
ERFeCr‑A6 | 3.0–5.0 | 22–28 | 1.0–2.0 | ≤2.0 | --- | small | Bal | --- | small Mo | 55-60 |
ERFeMn‑A | 0.8–1.4 | ≤4 | 12–16 | ≤1.5 | --- | --- | Bal | --- | --- | 45-55 |
ERCoCr‑A (Stellite 6) | 0.7–1.4 | 25–32 | ≤1.0 | ≤2.0 | 3-6 | ≤3 | ≤4 | Bal | --- | 40-45 |
ERCoCr‑B (Stellite 12) | 1.3–1.8 | 28–32 | ≤1.0 | ≤2.0 | 7–9.5 | ≤3 | ≤4 | Bal | --- | 48-53 |
ERCoCr‑C (Stellite 1) | 2.0–2.8 | 30–34 | ≤1.0 | ≤2.0 | 10–14 | ≤3 | ≤3 | Bal | --- | 51-56 |
ERNiCr‑C | 0.4–0.8 | 28–35 | ≤1.5 | ≤2.0 | --- | Bal | ≤8 | --- | --- | 38-44 |
ERNiCrFe‑A | ≤0.35 | 20–28 | ≤1.5 | ≤2.0 | --- | Bal | 15–25 | --- | --- | 30-38 |
ERWC‑A | Matrix C ~0.3–0.8 | 8–12 | ≤1.5 | ≤2.0 | WC particles | ≤5 | Bal | --- | WC particles 40–60% by weight | Matrix 40–50; WC >70 |
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Down Load
![]() Hardfacing Surfacing Wire.pdf
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Specifications
Type | Spool (MIG) | Tube (TIG) |
Specification ( MM ) | 0.8、0.9、1.0、1.2、1.6、2.0 | 1.6、2.0、2.4、3.2、4.0、5.0 |
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire video
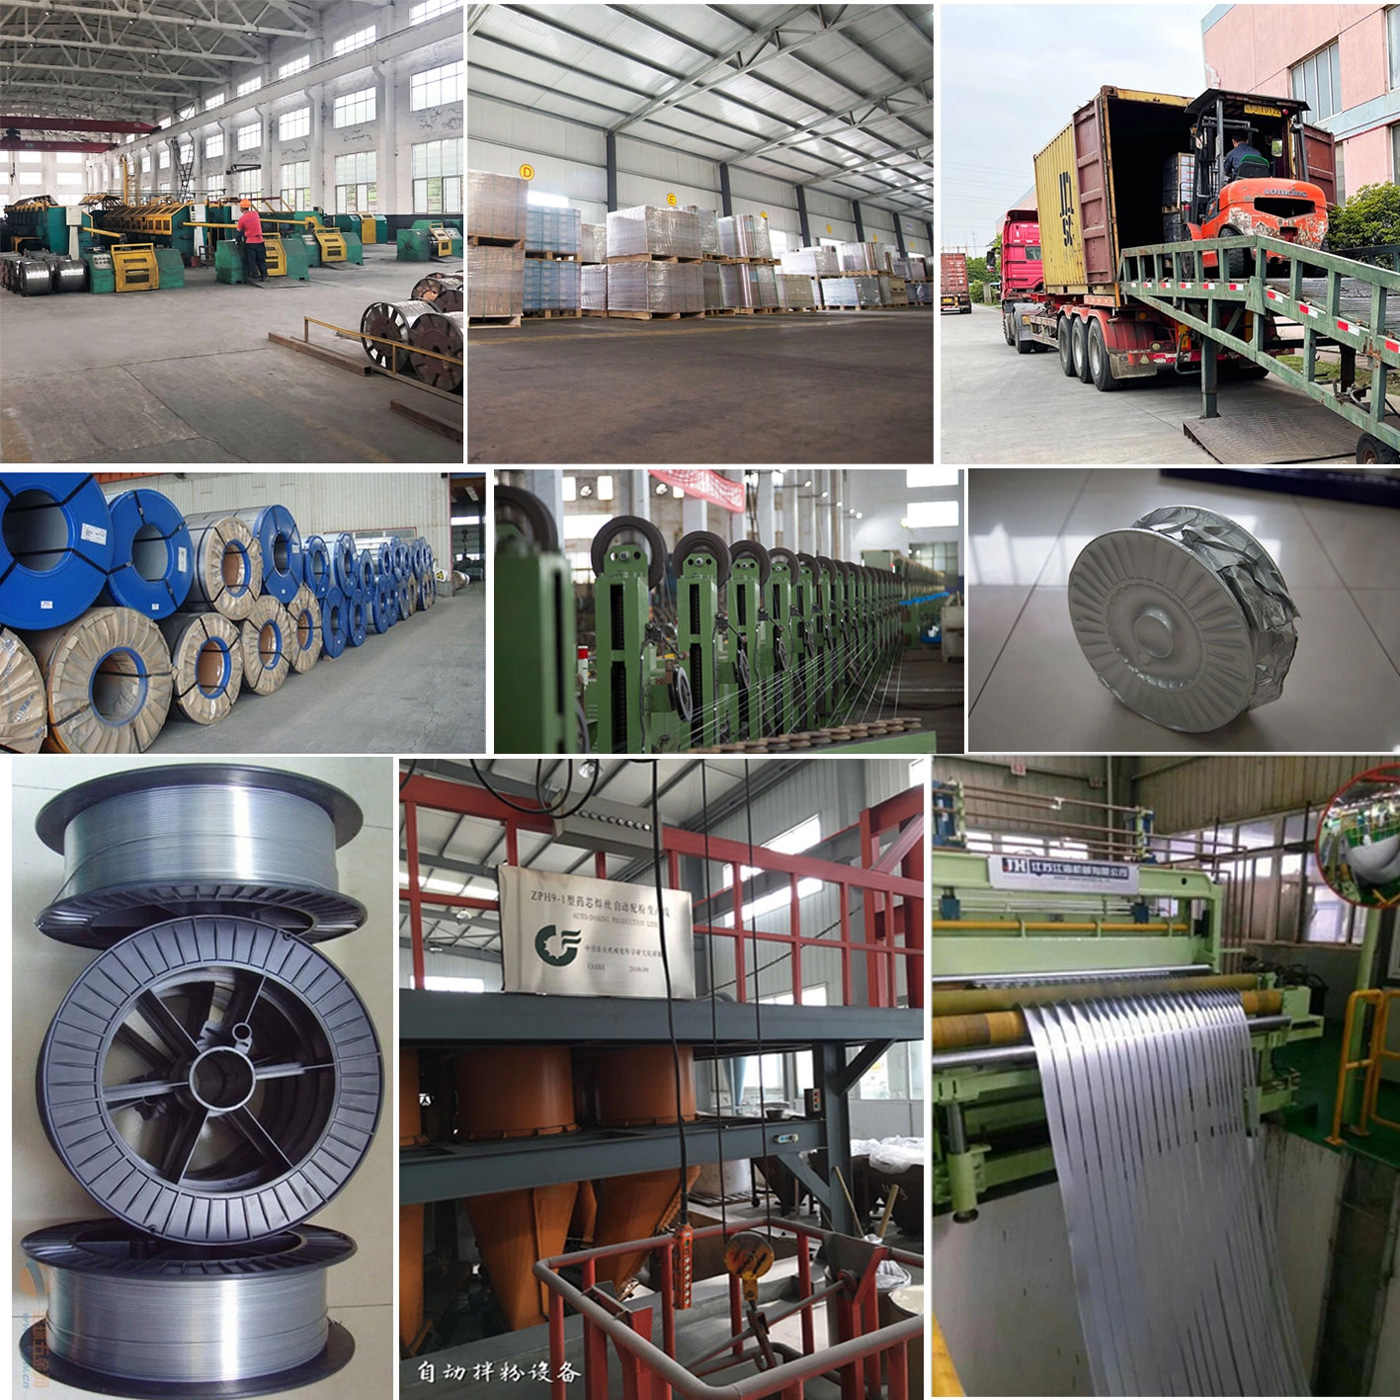
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Factory Show
![AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire]()
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Application
AWS A5.13‑A5.21 flux cored hardfacing surfacing wire is used for wear-resistant overlay and dimension rebuilding on mining, cement, power, valve, turbine and heavy machinery components.
![AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire]()
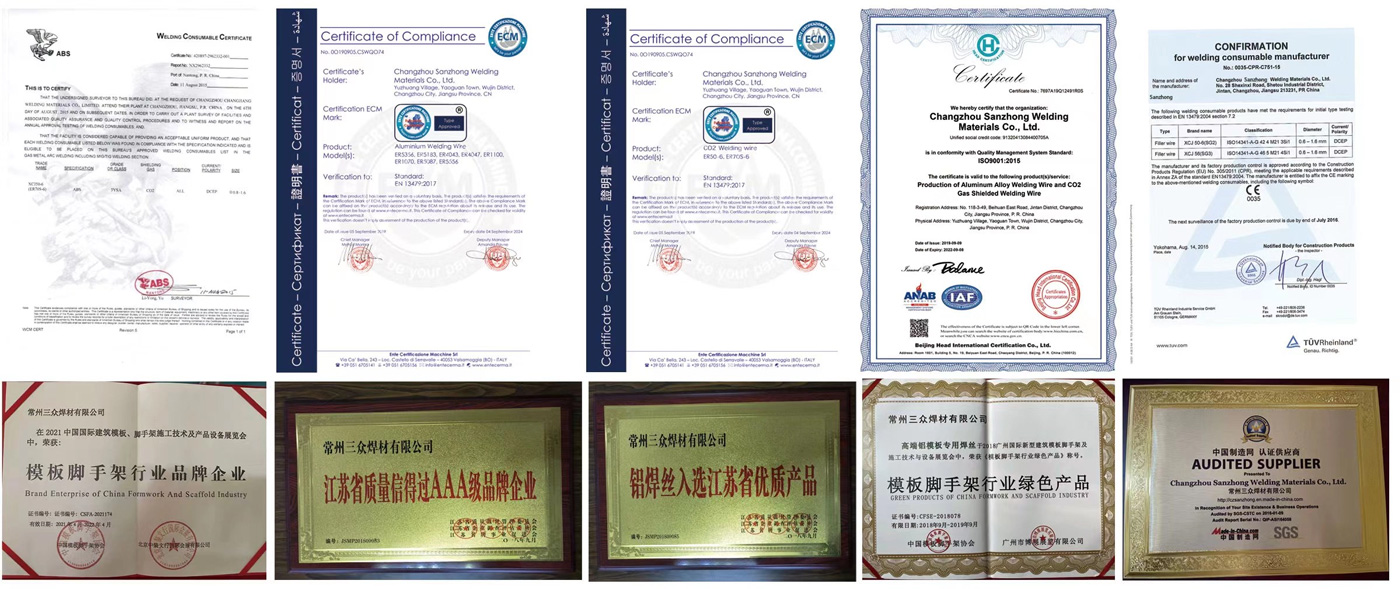
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire Certification
![AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire]()
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire WHAT YOU GET
best AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire
Choose Your stainless flux core wire Size in mm: 0.8mm / 0.9mm / 1.0mm / 1.2mm/ 1.6mm
Choose flux cored Hardfacing Surfacing Wire Size in inch: 0.030 / 0.035 / 0.040 / 0.045/ 0.063/ 3/16
Choose Your flux cored Hardfacing Surfacing Wire Spool Weight(Package): 0.5kg / 2kg / 7kg
Choose Your flux cored Hardfacing Surfacing Wire Size: 1.2mm/ 1.6mm/ 2.0mm
Choose Your Wire tube Weight(Package): 2kg / 5kg / 10kg / 1LB / 2LB / 4.5LB / 15.5LB / 20LB
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire knowledge
ERFeCr-A1,ERFeCr-A5,ERFeCr-A6,ERFeMn-A,ERCoCr-A,ERCoCr-C,ERNiCr-C,ERWC-A,ERCoCr-B,ERNiCrFe-A Requirements
1. Classification based on deposited weld metal chemical composition(for flux-cored/tubular wire), or base rod composition (solid bare rod).
2. Chemical composition limits for weld deposit: C, Mn, Si, Cr, Ni, Mo, W, Fe, S ≤0.035%, P ≤0.035%, total other impurities ≤1.0%.
3. Marking: Each spool/rod bundle must mark AWS classification, heat/lot number, manufacturer, diameter, traceability for MTC.
4. Packaging: Clean, dry packaging; vacuum packaging optional for high-alloy grades to prevent surface oxidation.
5. Physical attributes: Uniform wire diameter, no cracks, seams, scale, rust or surface defects; consistent rod straightness.
6. Test requirements: Chemical analysis per heat/lot; hardness test on deposited surfacing layer; visual weld bead inspection.
7. Weld deposit dilution control: TIG/MIG/FCAW surfacing shall be controlled to minimize base metal dilution to guarantee target alloy & hardness.
Grade by Grade Spec & Requirements
1. ERFeCr‑A1 (Iron‑Chromium Martensitic Surfacing Wire/Rod)
Deposit chemistry: C ~1.5–3.5%, Cr 8–14%, Mn 0.5–1.5%, Si ≤2.0%, balance Fe; S≤0.035, P≤0.035
Hardness: HRC 45–52
Requirement: Balanced abrasion + moderate impact resistance; not for heavy shock loads.
Application: Bucket teeth, fan blades, roll build-up, excavator wear parts.
2. ERFeCr‑A5 (Hypereutectic High Cr-C Iron Surfacing Wire/Rod)
Deposit chemistry: C 3.5–6.0%, Cr 24–32%, Mn 0.5–1.5%, Si ≤2.0%, Ni ≤4%, Mo ≤4%, balance Fe; S≤0.035, P≤0.035
Hardness: HRC 58–64
Requirement: Excellent low-stress abrasive wear; brittle, avoid heavy impact.
Application: Cement mill liners, chutes, hoppers, sand pump impellers.
3. ERFeCr‑A6 (High Chromium Iron, Improved Impact Tolerance)
Deposit chemistry: C 3.0–5.0%, Cr 22–28%, Mn 1.0–2.0%, Si ≤2.0%, small Ni/Mo addition, balance Fe
Hardness: HRC 55–60
Requirement: High abrasion resistance with slightly better toughness than ERFeCr‑A5; still limited impact capacity.
Application: Sinter plant parts, slag conveyors, powder handling equipment.
4. ERFeMn‑A (Hadfield Austenitic Manganese Surfacing Wire/Rod)
Deposit chemistry: C 0.8–1.4%, Mn 12–16%, Si ≤1.5%, Cr ≤4%, balance Fe
Hardness: As-deposited ~HRC 20–25; work-hardens up to HRC 45–55 under impact
Requirement: Work-hardening austenite; designed for heavy impact, poor resistance to fine abrasive wear.
Application: Jaw crusher plates, impactor blow bars, rail crossing, hammer heads.
5. ERCoCr‑A (Stellite 6, Cobalt Base)
Deposit chemistry: C 0.7–1.4%, Cr 25–32%, W 3–6%, Fe ≤4%, balance Co
Hardness: HRC 40–45
Requirement: Retain hardness up to ~650°C; good hot hardness, cavitation, corrosion & moderate wear resistance.
Application: Valve seats, turbine blades, hot shear knives, high temp valve trim.
6. ERCoCr‑B (Stellite 12, Cobalt Base)
Deposit chemistry: C 1.3–1.8%, Cr 28–32%, W 7–9.5%, Fe ≤4%, balance Co
Hardness: HRC 48–53
Requirement: Higher hardness than ERCoCr‑A; good hot abrasion, lower toughness.
Application: Hot forging dies, extrusion tools, high wear valve components.
7. ERCoCr‑C (Stellite 1, Cobalt Base)
Deposit chemistry: C 2.0–2.8%, Cr 30–34%, W 10–14%, Fe ≤3%, balance Co
Hardness: HRC 51–56
Requirement: Highest hardness among standard Stellite grades; brittle, excellent high-temperature abrasive wear.
Application: Hard cutting edges, high-wear valve inserts, drill tool overlay.
8. ERNiCr‑C (Nickel‑Chromium Hardfacing Surfacing Wire/Rod)
Deposit chemistry: C 0.4–0.8%, Cr 28–35%, Fe ≤8%, balance Ni
Hardness: HRC 38–44
Requirement: Good high-temperature oxidation, corrosion & galling resistance; resistant to thermal cycling.
Application: Furnace rolls, heat treatment fixtures, high temp corrosion + wear parts.
9. ERNiCrFe‑A (Ni‑Cr‑Fe Surfacing Wire/Rod)
Deposit chemistry: C ≤0.35%, Cr 20–28%, Fe 15–25%, balance Ni
Hardness: HRC 30–38
Requirement: High toughness, corrosion resistance, dissimilar metal compatibility; lower hardness.
Application: Corrosion resistant overlay, dissimilar metal transition layers, chemical equipment repair.
10. ERWC‑A (Tungsten Carbide Composite Tubular Surfacing Wire/Rod)
Deposit requirement: Tungsten carbide granules embedded in iron/nickel matrix; WC particle size & content controlled per AWS A5.21 for tubular WC rods.
Hardness: Matrix HRC 40–50; WC particles >HRC 70
Requirement: Extreme abrasive wear resistance; avoid heavy impact to prevent WC spalling.
Application: Oilfield drill stabilizers, rock cutting tools, augers, sand slurry equipment.
ERFeCr-A1,ERFeCr-A5,ERFeCr-A6,ERFeMn-A,ERCoCr-A,ERCoCr-C,ERNiCr-C,ERWC-A,ERCoCr-B,ERNiCrFe-A Identification
1. ERFeCr‑A1
ID meaning: ER = bare surfacing rod/wire; FeCr = Iron‑Chromium alloy system; A1 = Class A1 iron‑chromium martensitic surfacing deposit.
Label mark: AWS A5.21 ERFeCr‑A1
Alloy family: Iron‑chromium martensitic hardfacing.
2. ERFeCr‑A5
ID meaning: ER = bare surfacing rod/wire; FeCr = Iron‑Chromium; A5 = Class A5 hypereutectic high chromium carbide deposit.
Label mark: AWS A5.21 ERFeCr‑A5
Alloy family: Hypereutectic high Cr‑C iron hardfacing.
3. ERFeCr‑A6
ID meaning: ER = bare surfacing rod/wire; FeCr = Iron‑Chromium; A6 = Class A6 modified high chromium iron deposit with improved toughness.
Label mark: AWS A5.21 ERFeCr‑A6
Alloy family: Modified high chromium iron hardfacing.
4. ERFeMn‑A
ID meaning: ER = bare surfacing rod/wire; FeMn = Iron‑Manganese; A = Class A austenitic Hadfield manganese deposit.
Label mark: AWS A5.21 ERFeMn‑A
Alloy family: Austenitic manganese work‑hardening surfacing.
5. ERCoCr‑A
ID meaning: ER = bare surfacing rod/wire; CoCr = Cobalt‑Chromium; A = Class A cobalt‑base (Stellite 6) deposit.
Label mark: AWS A5.21 ERCoCr‑A
Alloy family: Cobalt base (Stellite 6).
6. ERCoCr‑B
ID meaning: ER = bare surfacing rod/wire; CoCr = Cobalt‑Chromium; B = Class B cobalt‑base (Stellite 12) deposit.
Label mark: AWS A5.21 ERCoCr‑B
Alloy family: Cobalt base (Stellite 12).
7. ERCoCr‑C
ID meaning: ER = bare surfacing rod/wire; CoCr = Cobalt‑Chromium; C = Class C cobalt‑base (Stellite 1) deposit.
Label mark: AWS A5.21 ERCoCr‑C
Alloy family: Cobalt base (Stellite 1).
8. ERNiCr‑C
ID meaning: ER = bare surfacing rod/wire; NiCr = Nickel‑Chromium; C = Class C nickel‑chromium hardfacing deposit.
Label mark: AWS A5.21 ERNiCr‑C
Alloy family: Nickel‑chromium high temp wear & corrosion resistant.
9. ERNiCrFe‑A
ID meaning: ER = bare surfacing rod/wire; NiCrFe = Nickel‑Chromium‑Iron; A = Class A NiCrFe alloy surfacing deposit.
Label mark: AWS A5.21 ERNiCrFe‑A
Alloy family: Nickel‑chromium‑iron corrosion resistant overlay.
10. ERWC‑A
ID meaning: ER = bare tubular surfacing rod/wire; WC = Tungsten carbide composite; A = Class A tungsten carbide reinforced deposit.
Label mark: AWS A5.21 ERWC‑A
Alloy family: Tungsten carbide composite hardfacing.
ERFeCr-A1,ERFeCr-A5,ERFeCr-A6,ERFeMn-A,ERCoCr-A,ERCoCr-C,ERNiCr-C,ERWC-A,ERCoCr-B,ERNiCrFe-A Packaging
1. ERFeCr‑A1 / ERFeCr‑A5 / ERFeCr‑A6 (Iron‑chromium hardfacing wire/rod)
Standard spool or rod bundle. Vacuum packaging optional but strongly recommended for overseas export. No special fragility limit, avoid sharp objects scratching wire surface.
2. ERFeMn‑A (Hadfield manganese surfacing wire/rod)
Manganese alloy easily oxidizes; inner plastic anti-rust bag required. Keep sealed when not in use.
3. ERCoCr‑A / ERCoCr‑B / ERCoCr‑C (Stellite cobalt base)
High value cobalt alloy. Vacuum moisture barrier bag mandatory. Straight rod form usually packed in metal tins to prevent bending and surface damage.
4. ERNiCr‑A / ERNiCrFe‑A (Nickel‑base surfacing wire/rod)
High alloy nickel material, sensitive to surface contamination. Vacuum sealed inner bag, spool with protective cover.
5. ERWC‑A (Tungsten carbide composite tubular wire)
Special care: Do not squeeze or crush the wire. Deformation will crack internal WC particles. Vacuum sealed bag; rigid carton or metal box. Stacking load limit on carton label.
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire WARNING
gas shielded flux cored wire,Before use, read and understand the manufacturer's instructions, Material Safety Data Sheets (MSDSs), and your employer's safety practices.
stainless steel flux core wire types have too many kinds ,Keep your head out of the fumes.Use enough ventilation, exhaust at the arc, or both, to keep fumes and gases away from your breathing zone and the general area.Wear correct eye, ear, and body protection.
flux wire welder,Do not touch live electrical parts.See American National Standard, ANSI 249.1, Safety in Welding.
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire FAQ
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire 10 famous brand are which factory?
1:sanzhong, 2:giant, 3:bohler, 4:rural king, 5:lincoln, 6:hyundai, 7:blue demon, 8:esab, 9:Oxford, 10:golden bridge
AWS A5.13-AWS A5.21-flux cored Hardfacing Surfacing Wire supplier and factories or wholesale locates in such countries like?
China,America,Brazil,England,Russia,Poland,India,Pakistan,NewZealand,Korea,Australia,Dubai,Turkey,Indonesia,UAE.
What is hardfacing flux cored wire?
Hardfacing flux cored wire is a tubular welding wire filled with alloy powders. It deposits wear-resistant overlay layer on metal surface via semi-automatic or automatic FCAW welding, widely used for surfacing repair of heavy machinery parts.
Difference between hardfacing flux cored wire and solid surfacing wire?
Flux cored surfacing wire has higher deposition efficiency, better bead forming and suitable for large area overlay. Solid surfacing wire produces lower dilution and fits precision small-area repair by TIG/MIG.
What is hypereutectic high chromium hardfacing wire used for?
Hypereutectic high chromium flux cored wire delivers very high hardness and excellent low-stress abrasive wear resistance. It is commonly used for cement mill, chute, hopper and powder conveying equipment, but not suitable for heavy impact working conditions.
What is Stellite cobalt based surfacing wire good for?
Stellite cobalt based surfacing wire maintains stable hardness under high temperature, with good cavitation, corrosion and hot wear resistance. It is widely used for valve seat, hot forging die and turbine component surfacing.
Hardfacing & Surfacing Flux Cored Wires + Related Special Welding Consumables?
1. Hardfacing Flux Cored Wires (FCAW Surfacing Wires)
Hardfacing flux cored wire is the most popular surfacing consumable for automatic / semi-automatic overlay welding. It uses a metal sheath filled
with alloy powder, easy operation, high deposition efficiency, good bead shape and adjustable alloy formula. Most can be used with CO₂ or mixed gas shielding;
some grades are self-shielded without external gas.
Main alloy series & typical grades
1. Iron based martensitic hardfacing flux cored wire
Grades: EFeCr-A1, EFeCr-A2, EFeCr-B, EFeMn-A
Features: Medium hardness, good balance of abrasion and impact resistance, low cost.
Application: Crusher hammers, shovel teeth, bucket teeth, rollers, fan blades, excavator parts, build-up of worn carbon steel components.
2. High chromium iron based (hypereutectic Cr-C) abrasion resistant flux cored wire**
Grades: EFeCrC-A, EFeCrC-B
Features: Very high hardness, excellent resistance to low-stress abrasive wear; brittle, not for heavy impact load.
Application: Cement mill liners, chute, hopper, sand pump impeller, slag conveyor, powder handling equipment.
3. Manganese austenitic hardfacing flux cored wire (Hadfield steel)**
Grades: EFeMn-A, EFeMn-B
Features: Work hardening property, high toughness under heavy impact, surface hardness rises after impact loading.
Application: Jaw crusher plates, impact crusher blow bars, railroad crossing, hammer subjected to strong impact.
4. Iron based high temperature & corrosion resistant surfacing flux cored wire**
Grades: EFeCrNi-A
Features: Resist high temperature oxidation and weak corrosion, stable performance at 500~650℃.
Application: Boiler tube, sintering machine parts, hot rolling mill guide.
5. Self-shielded hardfacing flux cored wire
Grades: E70T-4 hardfacing variant, self-shield EFeCr series
Features: No shielding gas required, suitable for field outdoor repair.
Application: On-site repair of mining machinery, mobile equipment in remote sites.
2. Cobalt based Surfacing Wires (Stellite)
Cobalt alloy (Stellite) surfacing consumables: flux cored wire, solid rod, stick electrode, PTA powder.
Grades: ECoCr-A, ECoCr-B, ECoCr-C, ERCoCr-A
Features: Outstanding hot hardness, high temperature wear resistance, cavitation resistance, corrosion resistance, keep hardness at high temperature.
Application: Valve seats, steam turbine blades, hot forging dies, injection screw, cutting tools, chemical equipment subjected to high temp wear & corrosion.
3. Nickel based Surfacing & Cladding Wires
Nickel alloy surfacing flux cored wire, metal cored wire, solid wire, stick electrode, cladding powder.
Grades: ENiCrMoT, ERNiCr, ENiCrFe, ENiCrMo-3 surfacing grade
Features: Excellent corrosion resistance in acid, chloride and high temperature environment; good toughness, anti-pitting, anti-crevice corrosion.
Application: Corrosion resistant overlay, chemical reactor, seawater equipment, dissimilar metal cladding, oil & gas valve, heat exchanger repair.
4. Metal Cored Surfacing Wires
Metal cored hardfacing wire (metal powder inside sheath, low slag or slag-free).
Features: High deposition rate, low spatter, smooth bead, suitable for robotic automatic surfacing, low slag easy multi-layer overlay.
Grades: FeCr metal cored series, NiCr metal cored series, CoCr metal cored series
Application: Robot automatic hardfacing, roll overlay, large batch component repair.
5. Solid Surfacing Welding Rods / Solid Surfacing Wires (GTAW / GMAW)
Solid hardfacing rods for TIG / MIG surfacing, AWS A5.21 standard.
Grades: ERCoCr-A, ERFeCr-A
Features: Low dilution, precise overlay thickness, suitable for small parts and fine repair.
Application: Die repair, small valve parts, precision component surfacing.
6. SMAW Stick Hardfacing Electrodes (Manual Surfacing Electrodes)
AWS A5.13 / A5.21 manual hardfacing covered electrodes.
Grades: EFeMn-A, ECoCr-A, ECrC-A
Features: Portable, no welding machine wire feeder needed, convenient for small local field repair.
Application: Local defect repair, small workshop manual hardfacing.
7. Surfacing Powders for PTA & Laser Cladding (AWS A5.38)
Metal alloy powder for Plasma Transferred Arc (PTA) cladding and laser cladding, covered by AWS A5.38.
Alloy system: Iron-based, nickel-based, cobalt-based, WC composite powder.
Features: Ultra-low dilution, very fine overlay layer, high hardness and wear resistance, high precision cladding.
Application: Hydraulic piston, valve core, shaft sleeve, turbine parts, mold repair, aerospace precision components.
WC tungsten carbide powder: Extreme abrasive wear resistance, used for drill bit, oil tool, powder conveying equipment.
8. Composite Tungsten Carbide Hardfacing Consumables
WC reinforced flux cored wire, WC stick electrode, WC PTA powder.
Features: Hard tungsten carbide particles distributed in metal matrix, top performance against severe abrasive wear.
Application: Oil drill stabilizer, sand mill, mining auger, rock cutting tools.
AWS A5 Series Welding Consumables Full Introduction?
AWS A5.01 / A5.01M
Welding Consumables – Procurement of Filler Metals and Fluxes
This standard covers general procurement, ordering, inspection and certification requirements for all AWS A5 welding consumables. It defines MTC
material test certificate rules, lot traceability, sampling and acceptance guidelines for buyers and manufacturers. No welding wire/electrode grades, it is a
purchasing guideline standard.
AWS A5.02 / A5.02M
Specification for Filler Metal Standard Sizes, Packaging, and Physical Attributes
Defines standard wire diameters, rod lengths, spool sizes, packaging forms, labeling requirements and physical dimension tolerance for all welding filler
metals. It is a general specification
for packaging and dimension, not for alloy classification.
AWS A5.1 / A5.1M
Specification for Carbon Steel Electrodes for Shielded Metal Arc Welding (SMAW / Stick Electrode)
Covered manual stick electrodes for carbon steel general fabrication.
Main grades: E6010, E6011, E7014, E7016, E7018, E7018‑1, E7024.
Application: Structural steel, pipe welding, carbon steel pressure vessel, general steel construction.
AWS A5.2 / A5.2M
Specification for Carbon and Low-Alloy Steel Rods for Oxyfuel Gas Welding
Solid gas welding rods for oxy-acetylene welding of carbon steel and low alloy steel.
Main grades: R60, R60‑G.
Application: Small carbon steel repair, sheet metal oxyfuel joining.
AWS A5.3 / A5.3M
Specification for Aluminum and Aluminum-Alloy Electrodes for Shielded Metal Arc Welding
SMAW covered aluminium stick electrodes for aluminium manual arc welding.
Main grades: E1100, E3003, E4043.
Application: Aluminium casting repair, on-site aluminium maintenance where MIG/TIG is unavailable.
AWS A5.4 / A5.4M
Specification for Stainless Steel Electrodes for Shielded Metal Arc Welding
SMAW stainless steel covered stick electrodes.
Main grades: E308‑16, E308L‑16, E309‑16, E309L‑16, E316L‑16, E310‑16, E2209‑16.
Application: Stainless steel pipe, pressure vessel, food equipment, corrosion resistant stainless fabrication.
AWS A5.5 / A5.5M
Specification for Low-Alloy Steel Electrodes for Shielded Metal Arc Welding
SMAW low alloy steel stick electrodes for high strength and high temperature service.
Main grades: E7018‑A1, E8018‑B2, E9018‑B3, E8018‑C1, E9018‑C3, E10018‑D2.
Application: Boiler, power plant, high pressure pipeline, low temperature steel structural welds.
AWS A5.6 / A5.6M
Specification for Copper and Copper Alloy Electrodes for Shielded Metal Arc Welding
SMAW copper alloy covered stick electrodes.
Main grades: ECu, ECuSi, ECuSn, ECuAl‑A2.
Application: Copper casting repair, bronze, aluminium bronze corrosion equipment.
AWS A5.7 / A5.7M
Specification for Bare Copper and Copper Alloy Welding Electrodes and Rods
Solid copper alloy MIG/TIG welding wires and straight rods.
Main grades: ERCu, ERCuSi‑A, ERCuSn‑A, ERCuAl‑A1, ERCuAl‑A2.
Application: Heat exchanger, copper pipe, bronze components, marine copper alloy parts.
AWS A5.8 / A5.8M
Specification for Filler Metals for Brazing and Braze Welding
Brazing filler rods and wires for brazing process.
Main grades: BCu, BCuP, BAg, BAlSi.
Application: HVAC, carbide tip brazing, copper pipe brazing, aluminium brazing assembly.
AWS A5.9 / A5.9M
Specification for Bare Stainless Steel Welding Electrodes and Rods
Solid stainless steel MIG/TIG welding wires and rods.
Main grades: ER308, ER308L, ER309, ER309L, ER316L, ER310, ER2209.
Application: Stainless steel chemical equipment, seawater piping, duplex stainless structural parts.
AWS A5.10 / A5.10M
Specification for Bare Aluminum and Aluminum Alloy Welding Electrodes and Rods
Solid aluminium alloy MIG/TIG welding wires and straight rods.
Main grades: ER1100, ER4043, ER4047, ER5356, ER5183, ER3103, ER2219, ER2319.
Application: Aerospace, new energy structural components, aluminium casting repair, aluminium tank, heat exchanger. ER2319 (AlCu6MnZrTi) is heat-treatable
for high strength 2219 aluminium alloy.
AWS A5.11 / A5.11M
Specification for Nickel and Nickel Alloy SMAW Electrodes
SMAW nickel alloy covered stick electrodes.
Main grades: ENi‑1, ENiCrFe‑2, ENiCrMo‑3, ENiCrMo‑4, ENiCrMo‑10.
Application: Strong corrosive chemical reactor, dissimilar metal welding, high temperature equipment.
AWS A5.12 / A5.12M
Specification for Tungsten and Oxide Dispersed Tungsten Electrodes for Arc Welding
TIG tungsten electrodes (non-filler metal, arc ignition electrode).
Main grades: EWTh‑2, EWCe‑2, EWLa‑1.5, EWZr‑1, EWP.
Application: TIG welding for all metal materials.
AWS A5.13 / A5.13M
Specification for Surfacing Electrodes for SMAW
Manual stick hardfacing electrodes for wear resistant overlay.
Main grades: EFeMn‑A, ECoCr‑A, ECrC‑A.
Application: Mining machinery, crusher, valve seat, roll repair, abrasion resistant overlay.
AWS A5.14 / A5.14M
Specification for Bare Nickel and Nickel Alloy Welding Electrodes and Rods
Solid nickel alloy MIG/TIG welding wires and rods.
Main grades: ERNi‑1, ERNiCr‑3, ERNiCrMo‑3, ERNiCrMo‑4.
Application: High temperature, strong corrosion chemical equipment, dissimilar metal joining.
AWS A5.15 / A5.15M
Specification for Welding Electrodes and Rods for Cast Iron
Cast iron welding stick electrodes and filler rods.
Main grades: ENiFe‑CI, ENi‑CI, ESt, RCI.
Application: Grey cast iron, ductile iron casting defect repair, engine block repair.
AWS A5.16 / A5.16M
Specification for Bare Titanium and Titanium Alloy Welding Electrodes and Rods
Solid titanium MIG/TIG welding wires and rods.
Main grades: ERTi‑1, ERTi‑2, ERTi‑3, ERTi‑5 (Ti‑6Al‑4V).
ERTi‑1 is CP Ti Grade1 with maximum ductility; ERTi‑2 is general-purpose CP Ti Grade2; ERTi‑5 is high strength Ti‑6Al‑4V for aerospace.
All titanium wires require high purity argon shielding and vacuum packaging.
Application: Aerospace, chemical heat exchanger, seawater corrosion equipment, new energy lightweight parts.
AWS A5.17 / A5.17M
Specification for Carbon Steel Electrodes and Fluxes for Submerged Arc Welding
Carbon steel SAW solid wires matched with submerged arc fluxes.
Main grades: EM12K, EH12, EA2.
Application: Heavy steel plate fabrication, vessel longitudinal seam, structural steel SAW welding.
AWS A5.18 / A5.18M
Specification for Carbon Steel Electrodes and Rods for Gas Shielded Arc Welding
GMAW carbon steel solid MIG wires.
Main grades: ER70S‑2, ER70S‑3, ER70S‑6, ER70S‑7.
Application: General structural steel, steel frame, carbon steel component MIG welding.
AWS A5.19 / A5.19M
Specification for Magnesium Alloy Welding Electrodes and Rods
Solid magnesium alloy MIG/TIG welding wires.
Main grades: ERAZ61A, ERAZ92A, ERMgAl‑M.
Application: Magnesium alloy die casting repair, aerospace lightweight magnesium assemblies.
AWS A5.20 / A5.20M
Specification for Carbon Steel Flux Cored Welding Electrodes
Gas-shielded carbon steel FCAW flux cored wires.
Main grades: E70T‑1C, E71T‑8.
Application: High deposition rate structural steel fabrication, workshop automatic welding.
AWS A5.21 / A5.21M
Specification for Surfacing Welding Electrodes and Rods
Hardfacing filler metals including solid rod and flux cored wire for wear-resistant overlay.
Main grades: ERCoCr‑A, ECrC‑O.
Application: Hot wear, corrosion and abrasion resistant overlay for valve, turbine, mining parts.
AWS A5.22 / A5.22M
Specification for Stainless Steel Flux Cored and Metal Cored Welding Electrodes and Rods
Stainless steel gas shielded flux cored wires and metal cored wires.
Main grades: E308T‑1, E309T‑1, E316LT‑1, E2209T‑1.
Application: Stainless steel tank, pipe, corrosion resistant overlay, high efficiency stainless welding.
AWS A5.23 / A5.23M
Specification for Low-Alloy Steel Electrodes and Fluxes for Submerged Arc Welding
Low alloy steel SAW wires matched with submerged arc fluxes.
Main grades: EA1, EB2, EB3.
Application: Boiler steel, high temperature pressure vessel, low temperature heavy plate SAW welding.
AWS A5.24 / A5.24M
Specification for Nickel Alloy Flux Cored Welding Electrodes
Nickel alloy gas shielded flux cored wires.
Main grades: ENiCrMo3T0‑4.
Application: Strong corrosive medium, high temperature equipment, dissimilar metal welds.
AWS A5.25 / A5.25M
Specification for Low Alloy Steel Electrodes for Electroslag Welding
Electroslag welding consumables for thick low alloy steel plate.
Main grades: ESW‑1, ESW‑2.
Application: Ultra thick steel plate vertical electroslag welding for heavy machinery.
AWS A5.26 / A5.26M
Specification for Carbon and Low-Alloy Steel Electrodes for Electrogas Welding
Electrogas welding electrodes for vertical continuous welding of thick steel plate.
Application: Tall steel structure vertical seam welding.
AWS A5.27 / A5.27M
Specification for Carbon Steel Flux Cored Electrodes for Self-Shielded FCAW
Self-shielded carbon steel flux cored wires, no external shielding gas required.
Main grades: E71T‑8, E70T‑11.
Application: Outdoor site welding, field construction where argon/CO2 gas is inconvenient.
AWS A5.28 / A5.28M
Specification for Low-Alloy Steel Electrodes and Rods for Gas Shielded Arc Welding
Low alloy steel solid MIG/TIG wires.
Main grades: ER80S‑B2, ER90S‑B3, ER80S‑Ni1.
Application: High temperature boiler steel, low temperature pressure vessel, high strength low alloy steel components.
AWS A5.29 / A5.29M
Specification for Low-Alloy Steel Flux Cored Welding Electrodes
Gas shielded low alloy steel flux cored wires.
Main grades: E80T5‑B2, E91T1‑B3.
Application: High efficiency welding of high temperature and low temperature low alloy steel.
AWS A5.30 / A5.30M
Specification for Consumable Inserts
Consumable inserts for electroslag welding, not welding wire or electrode.
Application: ESW thick plate welding.
AWS A5.31 / A5.31M
Specification for Fluxes for Brazing and Braze Welding
Brazing flux, matched with brazing filler metal.
Application: Aluminium, copper, steel brazing.
AWS A5.32 / A5.32M
Specification for Fluxes for Soldering
Soft soldering flux for low temperature soldering.
AWS A5.33 / A5.33M
Specification for Soldering Fillers
Soft solder wire and solder bar for electronics soldering.
AWS A5.34 / A5.34M
Specification for Nickel Alloy Metal Cored Welding Wire
Nickel alloy metal cored GMAW wires.
Main grades: ENiCrMo3T0‑4, ENiCrMo4T0‑4.
Application: High efficiency MIG welding of nickel alloy for chemical and power industry.
AWS A5.35 / A5.35M
Specification for Aluminum Alloy Flux Cored Welding Electrodes
Aluminium alloy flux cored wires for aluminium welding.
Main grades: ER5XXXT‑X series aluminium flux cored wires.
Application: High efficiency aluminium MIG welding, aluminium casting repair.
AWS A5.36 / A5.36M
Specification for Magnesium Alloy Flux Cored Welding Electrodes
Magnesium alloy flux cored wires.
Application: High efficiency welding of magnesium alloy die castings.
AWS A5.38 / A5.38M
Specification for Plasma Transferred Arc and Laser Cladding Powders for Surfacing
Metal powder for PTA cladding and laser cladding, not wire or stick electrode.
Types: Iron-based, nickel-based, cobalt-based hardfacing powder.
Application: Valve, turbine shaft, hydraulic part laser cladding and PTA overlay for wear & corrosion resistance.
AWS A5.39 / A5.39M
Specification for Flux and Electrode Combinations for Submerged Arc and Electroslag Joining and Surfacing of Stainless Steel and Nickel Alloys
Combined standard for SAW flux + electrode matched set for stainless steel and nickel alloy submerged arc welding.
Application: Thick stainless steel and nickel alloy plate SAW welding for chemical and marine equipment.
The AWS A5 series filler metal system covers nearly all mainstream welding consumables for ferrous and non-ferrous metals. Users can select SMAW stick
electrodes, GMAW solid wires,
FCAW flux-cored wires, metal-cored wires, SAW wires & fluxes, brazing fillers and cladding powders according to base material, mechanical requirement,
service temperature, corrosion
environment and welding process.
Correct selection of AWS classified welding consumables ensures stable weld metal mechanical performance, corrosion resistance and long-term service
reliability for critical industrial projects.
AWS A5 series standards define welding electrodes, solid wires, flux cored wires, rods, fluxes and cladding powders for carbon steel, low alloy steel, stainless
steel, aluminium, copper, nickel,titanium, magnesium and cast iron welding, widely used in aerospace, chemical, marine and new energy industries.
Open Arc Self-Shielded Flux Cored Hardfacing Wire DIN 8555 and EN ISO 14700 including types?
DIN8555 EN ISO 14700 T Fe16(Cr-Nb)
DIN8555 EN ISO 14700 MF1-GZ-30-P
DIN8555 EN ISO 14700 MF1-GZ-35-P
DIN8555 EN ISO 14700 MF1-GZ-40-P
DIN8555 EN ISO 14700 MF2-GZ-45-G
DIN8555 EN ISO 14700 MF2-GZ-50-G
DIN8555 EN ISO 14700 MF3-GZ-50-GP
DIN8555 EN ISO 14700 MF3-GZ-55-GP
DIN8555 EN ISO 14700 MF4-GZ-20-P
DIN8555 EN ISO 14700 MF5-GZ-35-C
DIN8555 EN ISO 14700 MF5-GZ-40-C
DIN8555 EN ISO 14700 MF6-GF-55-G
DIN8555 EN ISO 14700 MF6-GF-60-G
DIN8555 EN ISO 14700 MF6-GF-65-G
DIN8555 EN ISO 14700 MF6-GF-70-G
DIN8555 EN ISO 14700 MF8-GZ-40-GC
DIN8555 EN ISO 14700 MF8-GZ-45-GC
DIN8555 EN ISO 14700 MF10-GF-60-G
DIN8555 EN ISO 14700 MF10-GF-65-G
DIN8555 EN ISO 14700 MF10-GF-70-G
DIN8555 EN ISO 14700 MF21-GF-60-G
DIN8555 EN ISO 14700 MF20-GZ-40-G
DIN8555 EN ISO 14700 MF20-GZ-45-G
DIN8555 EN ISO 14700 MF20-GZ-50-G
DIN8555 EN ISO 14700 E10-UM-65-G
DIN8555 EN ISO 14700 MSG1、MSG2、MSG3、
MSG4、MSG5、MSG6、MSG8、MSG10、MSG20、MSG21
DIN 8555 MF1-GZ-xx-P EN ISO 14700 T Fe1
DIN 8555 MF2-GZ-xx-G EN ISO 14700 T Fe2
DIN 8555 MF3-GZ-xx-GP EN ISO 14700 T Fe3
DIN 8555 MF4-GZ-20-P EN ISO 14700 T Fe4
DIN 8555 MF5-GZ-xx-C EN ISO 14700 T Fe5
DIN 8555 MF6-GF-60-G EN ISO 14700 T Fe8 equivalent to(UTP AF A60-O)
DIN 8555 MF8-GZ-xx-GC EN ISO 14700 T Ni1
DIN 8555 MF10-GF-65-G EN ISO 14700 T Z Fe15 equivalent to(UTP AF A43-O)
DIN 8555 MF20-GZ-xx-G EN ISO 14700 T Co1
DIN 8555 MF21-GF-xx-G EN ISO 14700 T Z Fe12
DIN 8555 E1-UM-xx-P EN ISO 14700 E Fe1
DIN 8555 E2-UM-xx-G EN ISO 14700 E Fe2
DIN 8555 E3-UM-xx-GP EN ISO 14700 E Fe3
DIN 8555 E4-UM-20-P EN ISO 14700 E Fe4
DIN 8555 E5-UM-xx-C EN ISO 14700 E Fe5
DIN 8555 E6-UM-60-G EN ISO 14700 E Fe8
DIN 8555 E8-UM-xx-GC EN ISO 14700 E Ni1
DIN 8555 E10-UM-65-G EN ISO 14700 E Fe15
DIN 8555 E20-UM-xx-G EN ISO 14700 E Co1
DIN 8555 E21-UM-xx-G EN ISO 14700 E Fe12
Welding consumables for hardfacing used for what position?
Excavator bucket teeth, crusher hammer, dredger parts, wear plate, screw conveyor, shredder, mining hardfacing
Hartauftragschweißen = Hartauftragsdraht
Hartauftragselektrode and Offener Lichtbogen Fülldraht named Auftragschweißen
wear resistance both also corrosion resistance position
Hardfacing welding consumables are used to deposit wear-resistant overlays on worn surfaces. Welding positions include flat, horizontal, vertical and overhead (subject to wire type). Typical products: crusher parts, excavator bucket teeth, auger flights, mill rollers, dozer blades, pump components, hot shear blades, shafts, gear teeth and railway crossings for mining, cement, dredging, steel and earthmoving industries.