Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Features
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)
Designed for welding heat treatable base alloys
Higher melting point and more fluidity
Suitable for sustained elevated temperature service
All position, include vertical down welding
Gray - white(post anodized) color
Standard: Zn98Al2 | Chemical Composition % |
| Zn | Al | Others | --- |
Grade Zn98Al2 | Rest | 1.8 ~ 2.2 | ≤ 0.3 | --- |
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)
![]() Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy).pdf
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Specifications
Type | Spool (MIG) | Tube (TIG) |
Specification ( MM ) | 0.8、0.9、1.0、1.2、1.6、2.0 | 1.6、2.0、2.4、3.2、4.0、5.0 |
Package | S100/1kg S200/5kg S270,S300/15kg-20kg | 5kg/box 10kg/box length :1000MM |
Mechanical Properties | Tensile Strength Mpa | Elongation after fracture A(%) |
--- | --- |
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) video
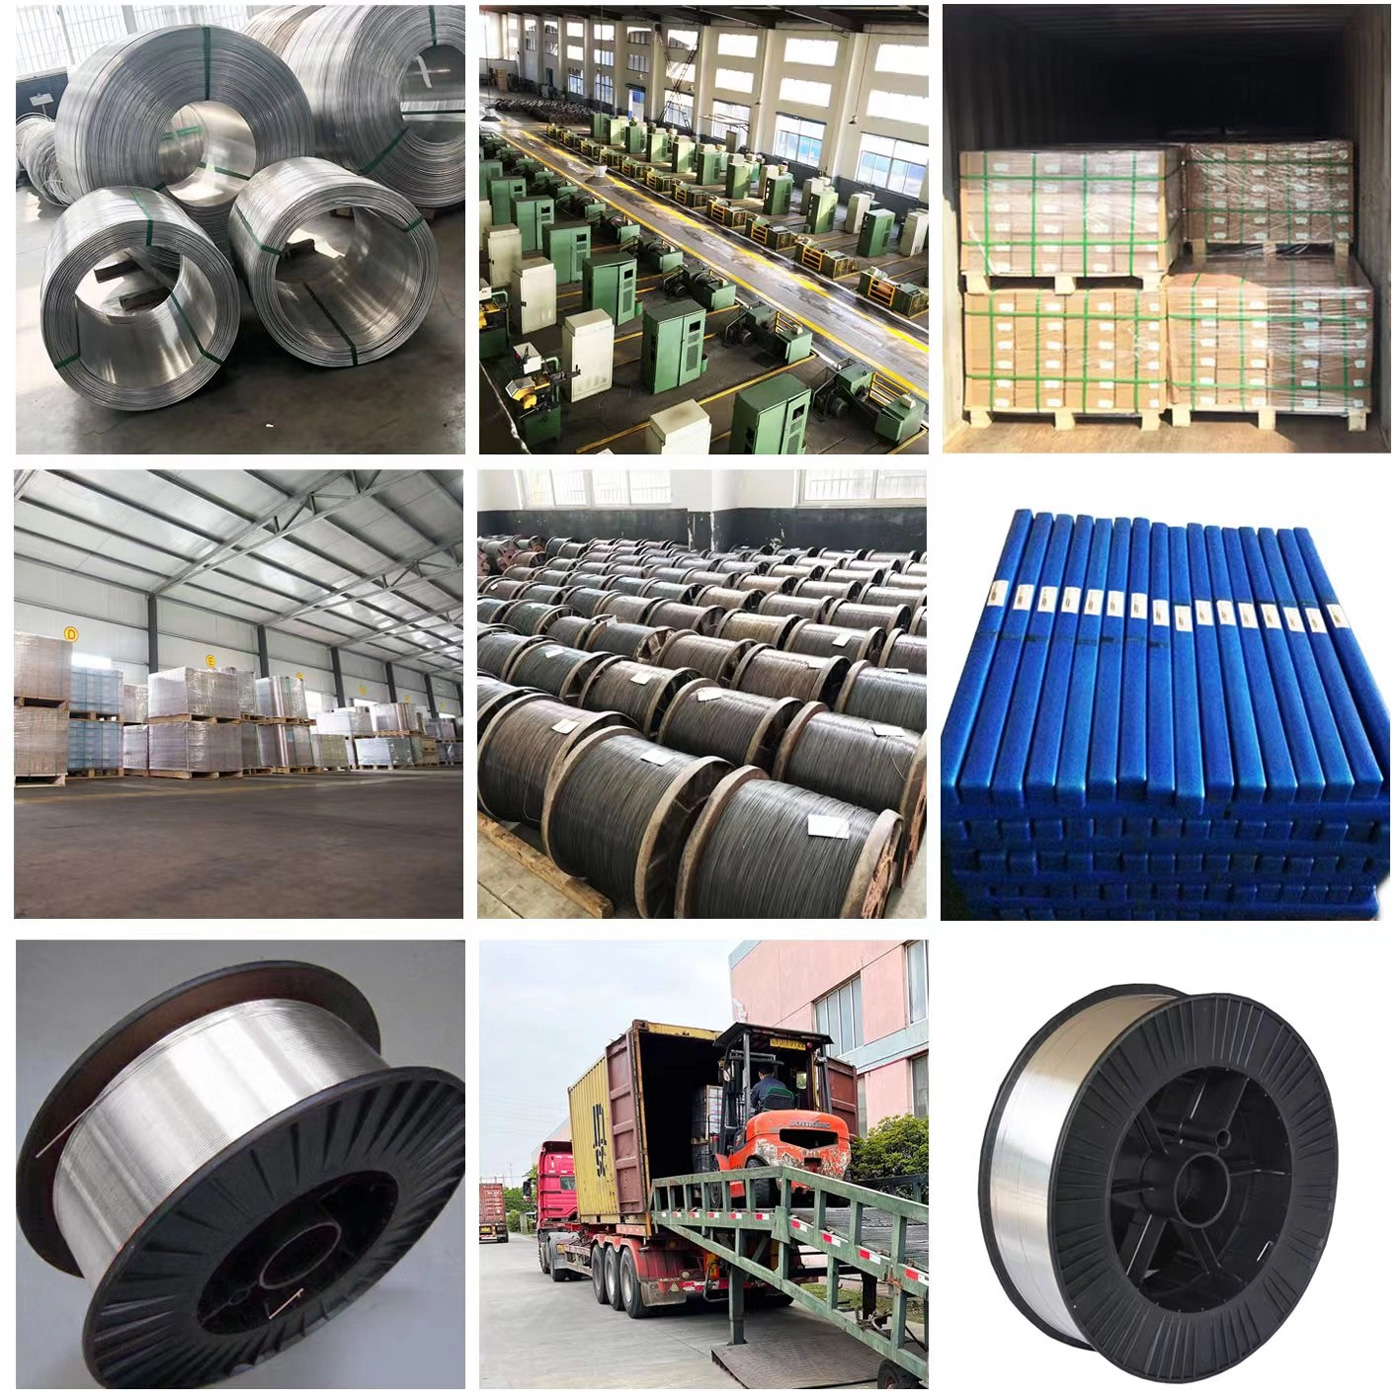
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Factory Show
![Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)]()
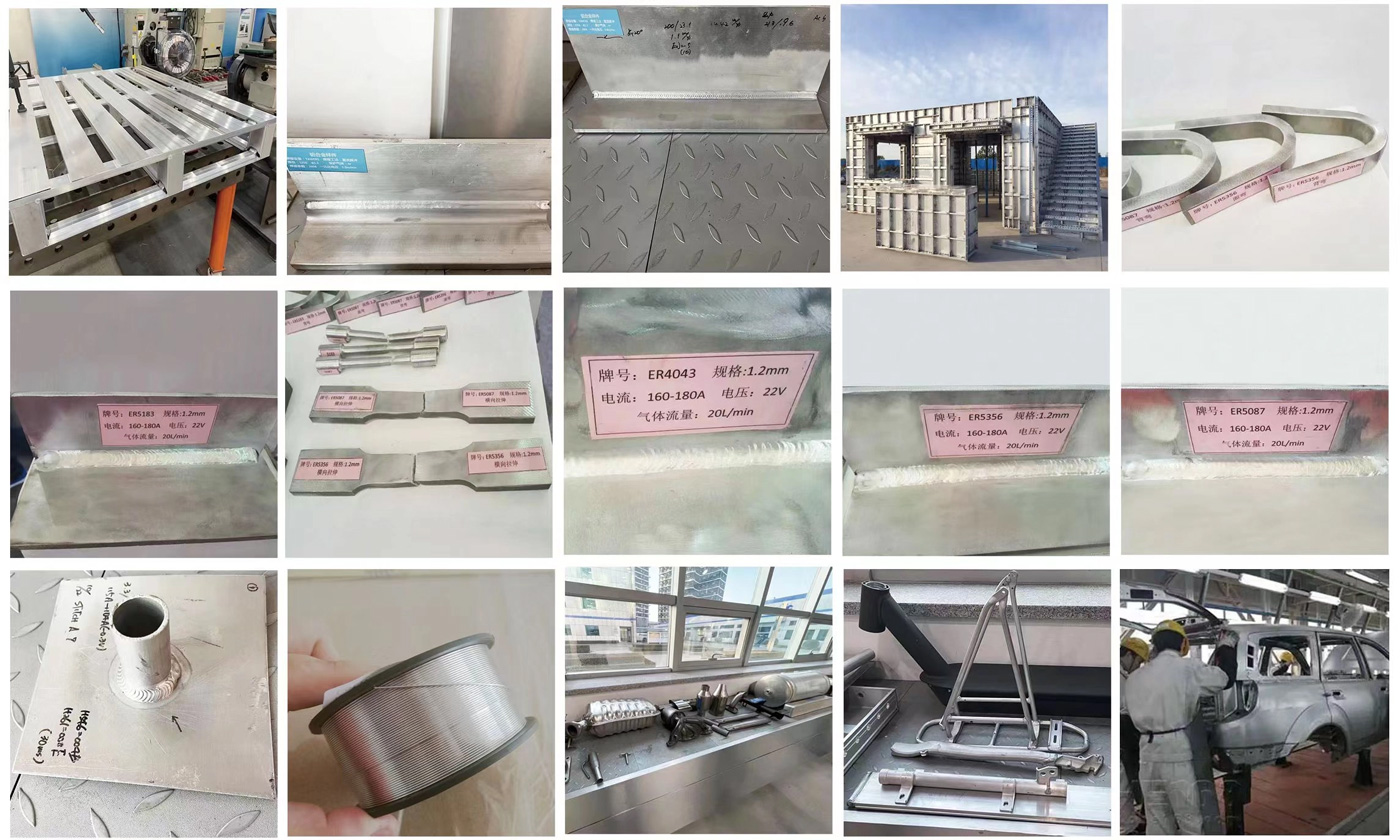
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Application
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) is used in railway locomotives,welding arc stability, beautiful welding, strong crack resistance. Welding operation and fluidity of molten gold are better.
![Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)]()
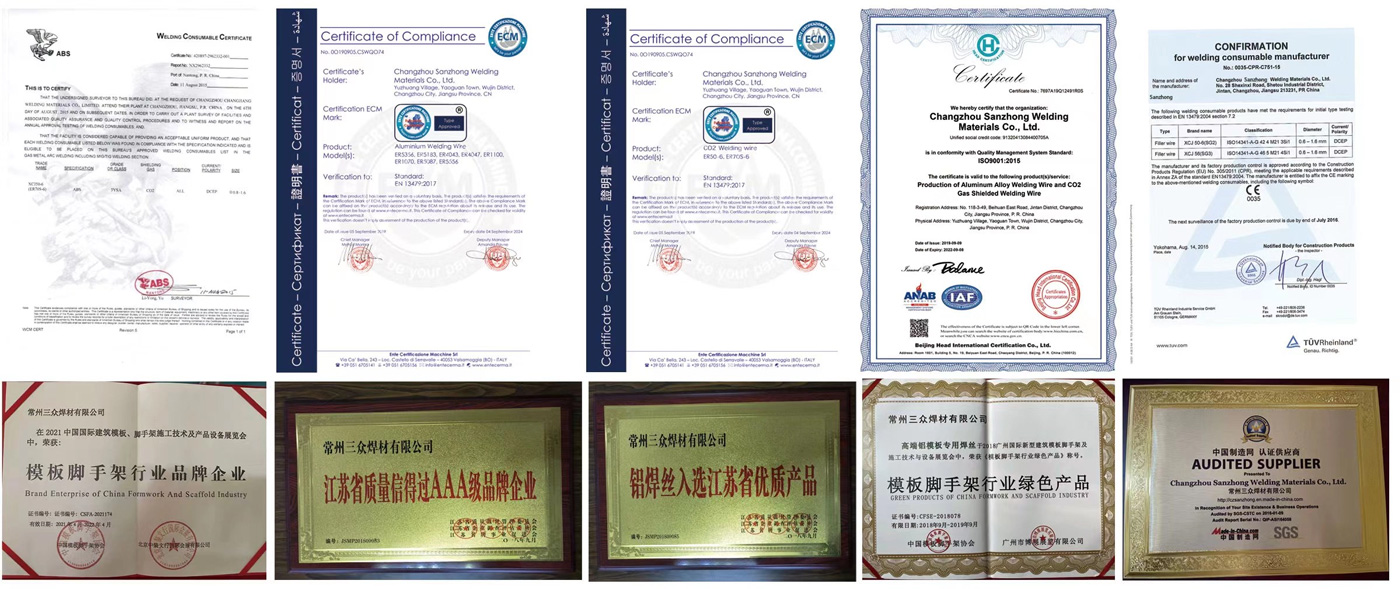
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Certification
![Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)]()
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) WHAT YOU GET
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)
Choose Flux Cored Brazing Wire AL02-Zn98Al2 Size in mm: 0.8mm / 0.9mm / 1.0mm / 1.2mm/ 1.6mm
Choose Flux Cored Brazing Wire AL02-Zn98Al2 Size in inch: 0.030 / 0.035 / 0.040 / 0.045/ 3/16 - 3/64
Choose Flux Cored Brazing Wire AL02-Zn98Al2 Spool Weight(Package): 0.5kg / 2kg / 7kg
Choose Flux Cored Brazing Wire AL02-Zn98Al2 Size: 1.2mm/ 1.6mm/ 2.0mm/ 2.4mm/ 3.2mm/ 4.0mm
Choose Flux Cored Brazing Wire AL02-Zn98Al2 Weight(Package): 5kg / 10kg / 1LB / 2LB / 4.5LB / 20LB
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) knowledge
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Requirements
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)
Flux Cored Brazing Wire AL02-Zn98Al2 is a self-fluxing Zn-Al alloy filler metal designed for dissimilar copper-to-aluminum brazing at 420–480°C with no extra brazing flux required.
AL02-Zn98Al2: Melting range 430~460°C; typical Cu-Al brazed lap joint tensile 80~110 MPa, shear 55~75 HV; no AWS A5.8 standard.
Melting range: 430 ~ 460 ℃
Recommended brazing temperature: 450 ~ 480 ℃
Good wettability and flowability on copper and aluminum substrates
Self-fluxing property, no extra brazing flux required during brazing operation
Recommended joint clearance: 0.08 ~ 0.13 mm
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Identification
Primary Use: Described as an "all-purpose workhorse alloy" for copper-based filler metals . Used for joining aluminum bronze, brass, steel, cast iron, and various dissimilar metals; also used for wear- and corrosion-resistant overlays .
Welding Processes: Designed for MIG (GMAW) and TIG (GTAW) welding .
Shielding Gas: Requires 100% Argon or an Argon/Helium mixture .
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) Packaging
Filler metal shall be suitably packaged to ensure against damage during shipment and storage under normal conditions.
The following product information (as a minimum of low temperature aluminum welding wire)
shall be legibly marked so as to be visible from the outside of each unit package:
(1) AWS specification and classification designation (year of issue may be excluded best wire for welding aluminum)
(2) Supplier's name and trade designation
(3) Size and net weight
(4) Lot, control, or heat number
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) WARNING
Welding fumes can be hazardous to your health. Work in a well-ventilated area or use a local exhaust (fume extraction) system to keep fumes away from your breathing zone .
Wear correct eye, ear, and body protection. Use welding goggles or a helmet with a shade 4-5 lens for gas welding , along with heat-resistant gloves and protective clothing . To avoid skin contact, follow standard precautions: wash thoroughly after handling, and do not allow contaminated work clothing to leave the worksite .
Avoid overheating. Excessive heat will cause zinc to evaporate from the alloy, producing excessive white fumes and leading to weld defects like porosity and reduced joint strength . Use a neutral or slightly oxidizing flame and control the heat input carefully to minimize zinc loss. Also, note that this filler metal is not suitable for furnace brazing in a controlled atmosphere due to zinc volatilization issues .
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) FAQ
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) 10 famous brand are which factory?
1:sanzhong, 2:giant, 3:safra, 4:Hobart, 5:SAF, 6:ALCOTEC, 7:INDALCO, 8:HYUNDAI, 9:Oxford, 10:golden bridge
Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy) supplier and factories locates in such countries like?
China,America,Brazil,England,Russia,Poland,India,Pakistan,NewZealand,Korea,Australia,Dubai,Turkey,Indonesia,UAE.
Flux Cored Brazing Wire AL02-Zn98Al2 VS ERCuSi-A?
AL02-Zn98Al2 flux cored brazing wire and ERCuSi-A serve completely different joining technologies. AL02-Zn98Al2 is a self-fluxing zinc-aluminum brazing filler metal for low-temperature dissimilar copper-to-aluminum brazing at 430~460°C, commonly used for heat exchangers. ERCuSi-A is AWS A5.7 silicon bronze solid welding wire for fusion welding of copper, brass and copper-to-steel. It cannot be used for copper-aluminum joining due to high melting temperature and brittle intermetallic formation. AL02 has no AWS classification, while ERCuSi-A is a standard AWS A5.7 classification.
Flux Cored Brazing Wire AL02-Zn98Al2 VS ERCuSn-A?
AL02-Zn98Al2 flux cored brazing wire and AWS A5.7 ERCuSn-A phosphor bronze welding wire belong to different joining categories. AL02-Zn98Al2 is a self-fluxing zinc-aluminum brazing filler metal for low-temperature dissimilar copper-to-aluminum brazing at 430~460°C, widely used for refrigeration heat exchangers. ERCuSn-A is solid phosphor bronze fusion welding wire for MIG/TIG welding of copper, brass, bronze and copper-to-steel components. It cannot be used for copper-aluminum joining because high welding heat creates brittle intermetallic layers. AL02 has no AWS classification, while ERCuSn-A is classified under AWS A5.7.
How is Flux Cored Brazing Wire AL02-Zn98Al2 applied for New Energy, Air Conditioning and Busbar customers, especially for PV Inverters and Energy Storage Copper-Aluminum Busbars?
Flux Cored Brazing Wire AL02-Zn98Al2 is a self-fluxing Zn-Al brazing filler metal for copper-to-aluminum dissimilar brazing.
For air conditioning: it joins copper tubes and aluminum fins / aluminum headers of heat exchangers.
For new energy & busbar industry: it is used to braze copper-aluminum transition joints of **PV inverters** and **energy storage Cu-Al busbars, forming reliable electrical connection between copper and aluminum.
Brazing works at 430~460°C; no additional brazing flux required. Suitable for flame brazing and induction brazing in mass production.
Air conditioning: Cu tube to Al fin/header brazing for heat exchangers
PV inverter: Copper to aluminum transition busbar joints
Energy storage: Dissimilar brazing of energy storage Cu-Al busbars
Self-fluxing, low brazing temperature 430~460°C, fit for mass production
How to choose a suitable Flux Cored Brazing Wire AL02-Zn98Al2, for Copper to Aluminum Brazing (Zn-Al alloy)?
When selecting AL02-Zn98Al2 flux cored brazing wire for copper-to-aluminum dissimilar brazing, first confirm your base metals are pure copper and aluminum/aluminum alloy. This self-fluxing Zn-Al brazing wire is suitable for flame brazing or induction brazing at 430–480°C. Check the joint clearance is controlled within 0.08~0.13 mm and ensure thorough cleaning of workpiece surfaces to remove oil, oxide and dirt. It is ideal for mass production of air conditioning heat exchangers, PV inverters and energy storage Cu-Al busbars. Note that AL02-Zn98Al2 is only for Cu-Al brazing, not for welding of other metal combinations.