AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Features
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire
ERTi‑1: CP Ti Gr.1, highest ductility & corrosion resistance, low strength
ERTi‑2: CP Ti Gr.2, general-purpose workhorse, balanced property
ERTi‑5: Ti‑6Al‑4V, high strength alpha-beta alloy for structural parts
All: AWS A5.16 solid wire, TIG/MIG, high purity argon shielding required
Bright silver / silvery-white-Straw / light gold(post anodized) color
Standard AWS A5.16 |
Chemical Composition % |
|
C |
O |
N |
H |
Fe |
Al |
V |
Ti |
OtherEach |
Other Total |
ERTi‑1 |
≤0.03 |
0.03~0.10 |
≤0.012 |
≤0.008 |
≤0.08 |
-- |
-- |
Rest |
≤ 0.05 |
≤0.15 |
ERTi‑2 |
≤0.03 |
0.08~0.16 |
≤0.015 |
≤0.008 |
≤0.12 |
-- |
-- |
Rest |
≤ 0.15 |
≤0.15 |
ERTi‑5 |
≤0.05 |
0.12~0.20 |
≤0.03 |
≤0.015 |
≤0.22 |
5.5~6.7 |
3.5~4.5 |
Rest |
≤ 0.15 |
≤0.15 |
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire
 AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire.pdf
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Specifications
Mechanical Properties |
Fusion Temperature ℃ |
Electrical IACS |
Density g/mm3 |
Tensile Mpa |
Yield Mpa |
Elongation % |
ERTi‑1 |
--- |
--- |
--- |
≥240 |
140~200 |
≥24 |
ERTi‑2 |
--- |
--- |
--- |
≥345 |
275~340 |
≥20 |
ERTi‑5 |
--- |
--- |
--- |
≥860 |
780~830 |
≥10 |
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire video
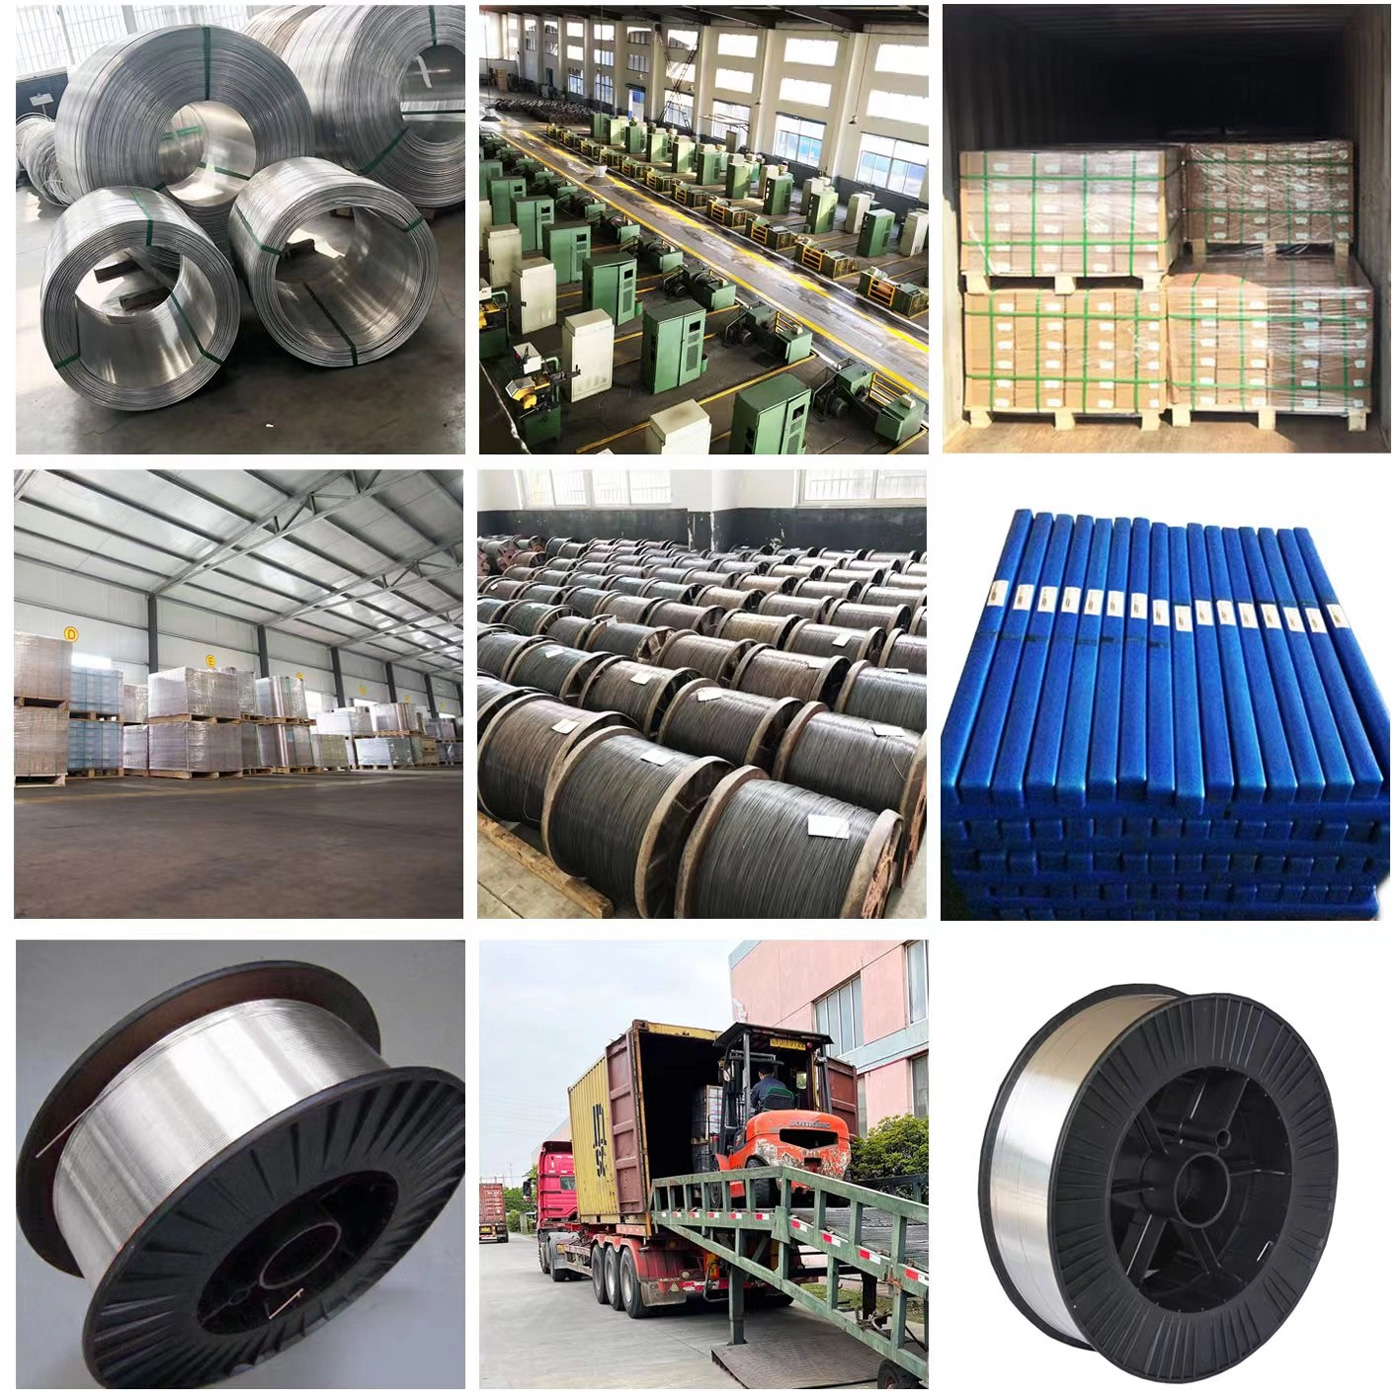
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Factory Show
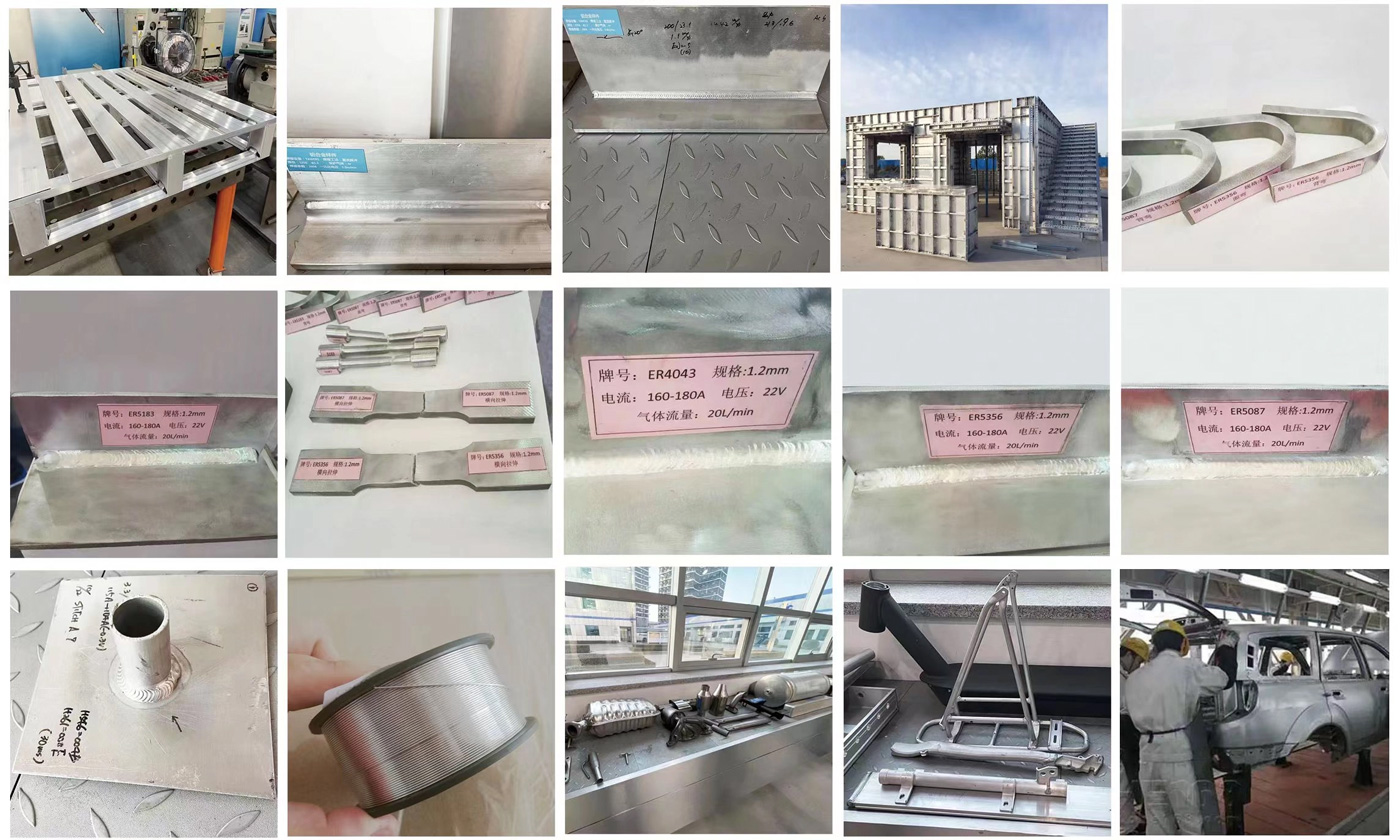
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Application
AWS A5.16 ERTi‑1 is for ductile Grade1 pure titanium corrosion equipment, widely used ERTi‑2 joins Grade1‑4 pure titanium for heat exchangers and chemical piping, while high strength ERTi‑5 (Ti‑6Al‑4V) is applied for aerospace and new energy load-bearing titanium alloy structures.
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Certification
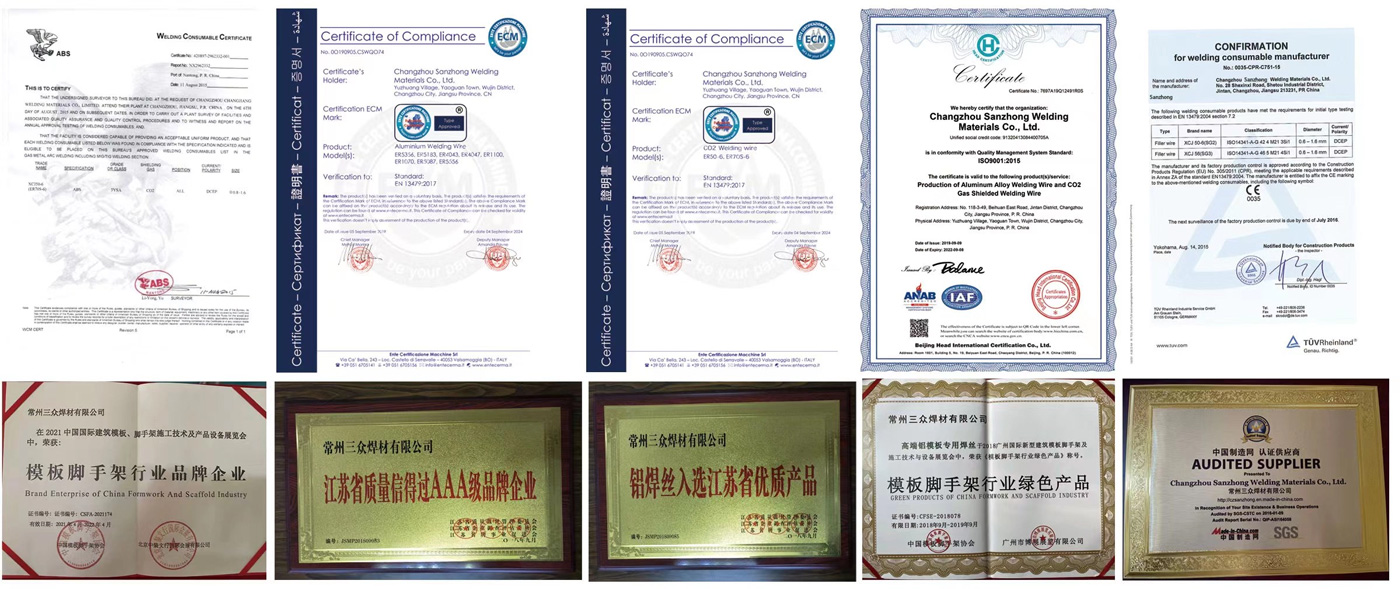
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire WHAT YOU GET
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire
Choose ERTi1 ERTi2 ERTi5 Titanium welding wire Size in mm: 0.8mm / 1.0mm / 1.2mm/ 1.6mm
Choose ERTi1 ERTi2 ERTi5 Titanium Size in inch: 0.030 / 0.035 / 0.040 / 0.045/ 3/16 - 3/64
Choose ERTi1 ERTi2 ERTi5 Titanium mig Spool Weight(Package): 0.5kg / 2kg / 7kg
Choose ERTi1 ERTi2 ERTi5 Titanium Size: 1.2mm/ 1.6mm/ 2.0mm/ 2.4mm/ 3.2mm/ 4.0mm
Choose ERTi1 ERTi2 ERTi5 Titanium Weight(Package): 5kg / 10kg / 1LB / 2LB / 4.5LB / 20LB
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire knowledge
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Requirements
ERTi‑1 (CP Titanium Grade1)
Softest commercially pure titanium filler, **maximum ductility**, lowest strength
Ultra-low interstitial elements; excellent corrosion resistance in oxidizing chemical environments
Good formability, ideal for welding Grade1 pure titanium
Low mechanical strength; not suitable for load-bearing structural parts
Applications: electrolytic equipment, deep-drawn titanium liners, explosion cladding
ERTi‑2 (CP Titanium Grade2)
Industry workhorse pure titanium wire; balanced strength, ductility and corrosion resistance
Most widely used CP Ti filler; matches Grade1/2/3/4 pure titanium
Good weldability, stable weld bead
Still pure titanium, strength much lower than Ti‑6Al‑4V
Applications: heat exchangers, chemical piping, pressure vessels, marine corrosion equipment
ERTi‑5 (Ti‑6Al‑4V, Grade5)
Alpha-beta titanium alloy filler, high strength & good toughness
High strength-to-weight ratio, heat treatable
Matched for welding Ti‑6Al‑4V titanium alloy
Higher cost; stricter welding procedure control
Applications: aerospace components, structural parts, power & new energy lightweight assemblies
AWS A5.16 ERTi‑1 and ERTi‑2 are commercially pure titanium solid wires. ERTi‑1 offers the highest ductility
and corrosion resistance for soft pure titanium components, while ERTi‑2 is the general-purpose grade with
balanced performance for chemical and heat exchanger fabrication. ERTi‑5 (Ti‑6Al‑4V) is alloyed titanium filler
delivering high strength for aerospace structural welds. All three wires require high-purity argon shielding to
prevent embrittlement of titanium weld metal.
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Identification
AWS A5.16 ERTi‑1, ERTi‑2 and ERTi‑5 titanium wires share similar silver-grey surface and cannot be told apart visually; identification depends on spool marking or chemical testing, while weld bead colour only monitors welding shielding quality.
Each spool / package shall be clearly marked:
AWS classification: ERTi‑1 / ERTi‑2 / ERTi‑5
Standard: AWS A5.16 / A5.16M
Alloy name: CP Ti Grade1 (ERTi‑1), CP Ti Grade2 (ERTi‑2), Ti‑6Al‑4V (ERTi‑5)
Wire diameter, net weight, heat / lot number, manufacturer name
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire Packaging
AWS A5.16 ERTi‑1, ERTi‑2 and ERTi‑5 titanium solid wires are vacuum-packed either on plastic spools for MIG or as 914mm straight rods for TIG,
with marked labels and MTC, to prevent oxygen and moisture contamination before welding.
MIG: Vacuum sealed plastic spool, 1/5/10kg
TIG: Vacuum sealed straight rod, standard length 914mm
Outer package: Carton + plywood case for export
Each unit marked with grade, size, lot number
Spooled wire (for GMAW / MIG)
Spool material: Plastic spool (D200 / D300 standard)
Net weight: 1kg, 5kg, 10kg per spool
Packing: Each spool vacuum-sealed in aluminium foil bag → carton box → plywood case for export
Available diameters: 0.8,1.0,1.2,1.6 mm
Straight cut rods (for GTAW / TIG)
Standard length: 914 mm (36 inch), optional 1000 mm
Diameters:1.6,2.0,2.4,3.2 mm
Packing: Vacuum sealed plastic tube / foil bag → plastic box → plywood case
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire WARNING
Welding fumes can be hazardous to your health. Work in a well-ventilated area or use a local exhaust (fume extraction) system to keep fumes away from your breathing zone .
Wear correct eye, ear, and body protection. Use welding goggles or a helmet with a shade 4-5 lens for gas welding , along with heat-resistant gloves and protective clothing . To avoid skin contact, follow standard precautions: wash thoroughly after handling, and do not allow contaminated work clothing to leave the worksite .
Avoid overheating. Excessive heat will cause zinc to evaporate from the alloy, producing excessive white fumes and leading to weld defects like porosity and reduced joint strength . Use a neutral or slightly oxidizing flame and control the heat input carefully to minimize zinc loss. Also, note that this filler metal is not suitable for furnace brazing in a controlled atmosphere due to zinc volatilization issues .
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire FAQ
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire 10 famous brand are which factory?
1:sanzhong, 2:giant, 3:safra, 4:Hobart, 5:SAF, 6:ALCOTEC, 7:INDALCO, 8:HYUNDAI, 9:Oxford, 10:golden bridge
AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire supplier and factories locates in such countries like?
China,America,Brazil,England,Russia,Poland,India,Pakistan,NewZealand,Korea,Australia,Dubai,Turkey,Indonesia,UAE.
Can ERTi‑1, ERTi‑2 and ERTi‑5 be substituted for each other?
Generally NO. ERTi‑1 and ERTi‑2 are commercially pure titanium fillers for CP titanium base metal. ERTi‑5 (Ti‑6Al‑4V) is high-strength alloy filler for Ti-6Al-4V. Mixing grades will lead to mismatched strength, corrosion resistance and cracking risk. Substitution requires engineering approval.
ERTi‑1 VS ERTi‑2 VS ERTi‑5?
AWS A5.16 ERTi‑1 and ERTi‑2 are commercially pure titanium solid wires. ERTi‑1 delivers the highest ductility and corrosion resistance with the lowest strength, for welding Grade1 pure titanium. ERTi‑2 is the most popular general-purpose pure titanium filler with balanced strength and corrosion resistance for Grade1~4 CP titanium. ERTi‑5 (Ti‑6Al‑4V) is alloyed titanium filler metal with much higher strength, designed for welding Ti‑6Al‑4V structural components. All three grades require high-purity argon shielding during TIG/MIG welding.
Titanium wire (ERTi‑1/ERTi‑2/ERTi‑5) VS Aluminum welding wires (AWS A5.10 ER2319, ER4043, ER5356, ER4145, ER2219, ER3103)?
Titanium solid wires have much higher strength and better corrosion resistance than aluminium fillers. ER2319 is high-strength Al-Cu heat-treatable wire for aerospace aluminium structures, but aluminium wires cannot match titanium’s performance in seawater and strong acid environments. Aluminium MIG/TIG wires only need argon shielding as well, but have no risk of high-temperature oxygen embrittlement like titanium.
Titanium wire (ERTi‑1/ERTi‑2/ERTi‑5) VS Copper alloy welding wires (AWS A5.7 ERCuSi-A, ERCuSn-A)?
Copper alloy wires have excellent thermal conductivity and are used for joining copper and bronze parts. Copper fillers have good wear resistance, but their corrosion resistance and strength-to-weight ratio are far below titanium. Copper alloy wires are not suitable for high-corrosion marine and chemical equipment.
Titanium wire (ERTi‑1/ERTi‑2/ERTi‑5) VS Nickel alloy welding wires (AWS A5.34 ERNiCrMo, ENiCrMo3T0-4, ENiCrMo3)?
Nickel-based fillers have great high-temperature corrosion resistance and can serve at elevated temperatures. Nickel alloy wires are heavier than titanium, with much higher density. Nickel fillers are chosen for high-temperature flue gas and strong oxidizing chemical conditions, while titanium works better at ambient / low temperature in chloride environment.
Titanium wire (ERTi‑1/ERTi‑2/ERTi‑5) VS Stainless steel solid wires (AWS A5.9 ER308L, ER309L, ER316L)?
Stainless steel wires are low-cost general corrosion fillers for piping and pressure vessels. Stainless steel suffers pitting corrosion in chloride seawater, while CP titanium (ERTi‑1, ERTi‑2) resists chloride pitting very well. Stainless steel density is higher than titanium and has poor strength-to-weight ratio for lightweight structures.
Titanium wire (ERTi‑1/ERTi‑2/ERTi‑5) VS Carbon steel / low alloy steel wires (AWS A5.18 ER70S‑6, AWS A5.28 ER80S‑Ni1)?
Carbon steel solid wires are low cost for structural steel fabrication, but rust easily in wet and marine environments. Carbon steel fillers have no corrosion resistance and cannot be used for corrosion-resistant equipment. Titanium is far more expensive but provides long service life under corrosive media.
AWS A5 Series Welding Consumables Full Introduction?
AWS A5.01 / A5.01M
Welding Consumables – Procurement of Filler Metals and Fluxes
This standard covers general procurement, ordering, inspection and certification requirements for all AWS A5 welding consumables.
It defines MTC material test certificate rules, lot traceability, sampling and acceptance guidelines for buyers and manufacturers. No welding wire/electrode
grades, it is a purchasing guideline standard.
AWS A5.02 / A5.02M
Specification for Filler Metal Standard Sizes, Packaging, and Physical Attributes
Defines standard wire diameters, rod lengths, spool sizes, packaging forms, labeling requirements and physical dimension tolerance for all welding filler
metals. It is a general specification for packaging and dimension, not for alloy classification.
AWS A5.1 / A5.1M
Specification for Carbon Steel Electrodes for Shielded Metal Arc Welding (SMAW / Stick Electrode)
Covered manual stick electrodes for carbon steel general fabrication.
Main grades: E6010, E6011, E7014, E7016, E7018, E7018‑1, E7024.
Application: Structural steel, pipe welding, carbon steel pressure vessel, general steel construction.
AWS A5.2 / A5.2M
Specification for Carbon and Low-Alloy Steel Rods for Oxyfuel Gas Welding
Solid gas welding rods for oxy-acetylene welding of carbon steel and low alloy steel.
Main grades: R60, R60‑G.
Application: Small carbon steel repair, sheet metal oxyfuel joining.
AWS A5.3 / A5.3M
Specification for Aluminum and Aluminum-Alloy Electrodes for Shielded Metal Arc Welding
SMAW covered aluminium stick electrodes for aluminium manual arc welding.
Main grades: E1100, E3003, E4043.
Application: Aluminium casting repair, on-site aluminium maintenance where MIG/TIG is unavailable.
AWS A5.4 / A5.4M
Specification for Stainless Steel Electrodes for Shielded Metal Arc Welding
SMAW stainless steel covered stick electrodes.
Main grades: E308‑16, E308L‑16, E309‑16, E309L‑16, E316L‑16, E310‑16, E2209‑16.
Application: Stainless steel pipe, pressure vessel, food equipment, corrosion resistant stainless fabrication.
AWS A5.5 / A5.5M
Specification for Low-Alloy Steel Electrodes for Shielded Metal Arc Welding
SMAW low alloy steel stick electrodes for high strength and high temperature service.
Main grades: E7018‑A1, E8018‑B2, E9018‑B3, E8018‑C1, E9018‑C3, E10018‑D2.
Application: Boiler, power plant, high pressure pipeline, low temperature steel structural welds.
AWS A5.6 / A5.6M
Specification for Copper and Copper Alloy Electrodes for Shielded Metal Arc Welding
SMAW copper alloy covered stick electrodes.
Main grades: ECu, ECuSi, ECuSn, ECuAl‑A2.
Application: Copper casting repair, bronze, aluminium bronze corrosion equipment.
AWS A5.7 / A5.7M
Specification for Bare Copper and Copper Alloy Welding Electrodes and Rods
Solid copper alloy MIG/TIG welding wires and straight rods.
Main grades: ERCu, ERCuSi‑A, ERCuSn‑A, ERCuAl‑A1, ERCuAl‑A2.
Application: Heat exchanger, copper pipe, bronze components, marine copper alloy parts.
AWS A5.8 / A5.8M
Specification for Filler Metals for Brazing and Braze Welding
Brazing filler rods and wires for brazing process.
Main grades: BCu, BCuP, BAg, BAlSi.
Application: HVAC, carbide tip brazing, copper pipe brazing, aluminium brazing assembly.
AWS A5.9 / A5.9M
Specification for Bare Stainless Steel Welding Electrodes and Rods
Solid stainless steel MIG/TIG welding wires and rods.
Main grades: ER308, ER308L, ER309, ER309L, ER316L, ER310, ER2209.
Application: Stainless steel chemical equipment, seawater piping, duplex stainless structural parts.
AWS A5.10 / A5.10M
Specification for Bare Aluminum and Aluminum Alloy Welding Electrodes and Rods
Solid aluminium alloy MIG/TIG welding wires and straight rods.
Main grades: ER1100, ER4043, ER4047, ER5356, ER5183, ER3103, ER2219, ER2319.
Application: Aerospace, new energy structural components, aluminium casting repair, aluminium tank, heat exchanger. ER2319 (AlCu6MnZrTi) is
heat-treatable for high strength 2219 aluminium alloy.
AWS A5.11 / A5.11M
Specification for Nickel and Nickel Alloy SMAW Electrodes
SMAW nickel alloy covered stick electrodes.
Main grades: ENi‑1, ENiCrFe‑2, ENiCrMo‑3, ENiCrMo‑4, ENiCrMo‑10.
Application: Strong corrosive chemical reactor, dissimilar metal welding, high temperature equipment.
AWS A5.12 / A5.12M
Specification for Tungsten and Oxide Dispersed Tungsten Electrodes for Arc Welding
TIG tungsten electrodes (non-filler metal, arc ignition electrode).
Main grades: EWTh‑2, EWCe‑2, EWLa‑1.5, EWZr‑1, EWP.
Application: TIG welding for all metal materials.
AWS A5.13 / A5.13M
Specification for Surfacing Electrodes for SMAW
Manual stick hardfacing electrodes for wear resistant overlay.
Main grades: EFeMn‑A, ECoCr‑A, ECrC‑A.
Application: Mining machinery, crusher, valve seat, roll repair, abrasion resistant overlay.
AWS A5.14 / A5.14M
Specification for Bare Nickel and Nickel Alloy Welding Electrodes and Rods
Solid nickel alloy MIG/TIG welding wires and rods.
Main grades: ERNi‑1, ERNiCr‑3, ERNiCrMo‑3, ERNiCrMo‑4.
Application: High temperature, strong corrosion chemical equipment, dissimilar metal joining.
AWS A5.15 / A5.15M
Specification for Welding Electrodes and Rods for Cast Iron
Cast iron welding stick electrodes and filler rods.
Main grades: ENiFe‑CI, ENi‑CI, ESt, RCI.
Application: Grey cast iron, ductile iron casting defect repair, engine block repair.
AWS A5.16 / A5.16M
Specification for Bare Titanium and Titanium Alloy Welding Electrodes and Rods
Solid titanium MIG/TIG welding wires and rods.
Main grades: ERTi‑1, ERTi‑2, ERTi‑3, ERTi‑5 (Ti‑6Al‑4V).
ERTi‑1 is CP Ti Grade1 with maximum ductility; ERTi‑2 is general-purpose CP Ti Grade2; ERTi‑5 is high strength Ti‑6Al‑4V for aerospace.
All titanium wires require high purity argon shielding and vacuum packaging.
Application: Aerospace, chemical heat exchanger, seawater corrosion equipment, new energy lightweight parts.
AWS A5.17 / A5.17M
Specification for Carbon Steel Electrodes and Fluxes for Submerged Arc Welding
Carbon steel SAW solid wires matched with submerged arc fluxes.
Main grades: EM12K, EH12, EA2.
Application: Heavy steel plate fabrication, vessel longitudinal seam, structural steel SAW welding.
AWS A5.18 / A5.18M
Specification for Carbon Steel Electrodes and Rods for Gas Shielded Arc Welding
GMAW carbon steel solid MIG wires.
Main grades: ER70S‑2, ER70S‑3, ER70S‑6, ER70S‑7.
Application: General structural steel, steel frame, carbon steel component MIG welding.
AWS A5.19 / A5.19M
Specification for Magnesium Alloy Welding Electrodes and Rods
Solid magnesium alloy MIG/TIG welding wires.
Main grades: ERAZ61A, ERAZ92A, ERMgAl‑M.
Application: Magnesium alloy die casting repair, aerospace lightweight magnesium assemblies.
AWS A5.20 / A5.20M
Specification for Carbon Steel Flux Cored Welding Electrodes
Gas-shielded carbon steel FCAW flux cored wires.
Main grades: E70T‑1C, E71T‑8.
Application: High deposition rate structural steel fabrication, workshop automatic welding.
AWS A5.21 / A5.21M
Specification for Surfacing Welding Electrodes and Rods
Hardfacing filler metals including solid rod and flux cored wire for wear-resistant overlay.
Main grades: ERCoCr‑A, ECrC‑O.
Application: Hot wear, corrosion and abrasion resistant overlay for valve, turbine, mining parts.
AWS A5.22 / A5.22M
Specification for Stainless Steel Flux Cored and Metal Cored Welding Electrodes and Rods
Stainless steel gas shielded flux cored wires and metal cored wires.
Main grades: E308T‑1, E309T‑1, E316LT‑1, E2209T‑1.
Application: Stainless steel tank, pipe, corrosion resistant overlay, high efficiency stainless welding.
AWS A5.23 / A5.23M
Specification for Low-Alloy Steel Electrodes and Fluxes for Submerged Arc Welding
Low alloy steel SAW wires matched with submerged arc fluxes.
Main grades: EA1, EB2, EB3.
Application: Boiler steel, high temperature pressure vessel, low temperature heavy plate SAW welding.
AWS A5.24 / A5.24M
Specification for Nickel Alloy Flux Cored Welding Electrodes
Nickel alloy gas shielded flux cored wires.
Main grades: ENiCrMo3T0‑4.
Application: Strong corrosive medium, high temperature equipment, dissimilar metal welds.
AWS A5.25 / A5.25M
Specification for Low Alloy Steel Electrodes for Electroslag Welding
Electroslag welding consumables for thick low alloy steel plate.
Main grades: ESW‑1, ESW‑2.
Application: Ultra thick steel plate vertical electroslag welding for heavy machinery.
AWS A5.26 / A5.26M
Specification for Carbon and Low-Alloy Steel Electrodes for Electrogas Welding
Electrogas welding electrodes for vertical continuous welding of thick steel plate.
Application: Tall steel structure vertical seam welding.
AWS A5.27 / A5.27M
Specification for Carbon Steel Flux Cored Electrodes for Self-Shielded FCAW
Self-shielded carbon steel flux cored wires, no external shielding gas required.
Main grades: E71T‑8, E70T‑11.
Application: Outdoor site welding, field construction where argon/CO2 gas is inconvenient.
AWS A5.28 / A5.28M
Specification for Low-Alloy Steel Electrodes and Rods for Gas Shielded Arc Welding
Low alloy steel solid MIG/TIG wires.
Main grades: ER80S‑B2, ER90S‑B3, ER80S‑Ni1.
Application: High temperature boiler steel, low temperature pressure vessel, high strength low alloy steel components.
AWS A5.29 / A5.29M
Specification for Low-Alloy Steel Flux Cored Welding Electrodes
Gas shielded low alloy steel flux cored wires.
Main grades: E80T5‑B2, E91T1‑B3.
Application: High efficiency welding of high temperature and low temperature low alloy steel.
AWS A5.30 / A5.30M
Specification for Consumable Inserts
Consumable inserts for electroslag welding, not welding wire or electrode.
Application: ESW thick plate welding.
AWS A5.31 / A5.31M
Specification for Fluxes for Brazing and Braze Welding
Brazing flux, matched with brazing filler metal.
Application: Aluminium, copper, steel brazing.
AWS A5.32 / A5.32M
Specification for Fluxes for Soldering
Soft soldering flux for low temperature soldering.
AWS A5.33 / A5.33M
Specification for Soldering Fillers
Soft solder wire and solder bar for electronics soldering.
AWS A5.34 / A5.34M
Specification for Nickel Alloy Metal Cored Welding Wire
Nickel alloy metal cored GMAW wires.
Main grades: ENiCrMo3T0‑4, ENiCrMo4T0‑4.
Application: High efficiency MIG welding of nickel alloy for chemical and power industry.
AWS A5.35 / A5.35M
Specification for Aluminum Alloy Flux Cored Welding Electrodes
Aluminium alloy flux cored wires for aluminium welding.
Main grades: ER5XXXT‑X series aluminium flux cored wires.
Application: High efficiency aluminium MIG welding, aluminium casting repair.
AWS A5.36 / A5.36M
Specification for Magnesium Alloy Flux Cored Welding Electrodes
Magnesium alloy flux cored wires.
Application: High efficiency welding of magnesium alloy die castings.
AWS A5.38 / A5.38M
Specification for Plasma Transferred Arc and Laser Cladding Powders for Surfacing
Metal powder for PTA cladding and laser cladding, not wire or stick electrode.
Types: Iron-based, nickel-based, cobalt-based hardfacing powder.
Application: Valve, turbine shaft, hydraulic part laser cladding and PTA overlay for wear & corrosion resistance.
AWS A5.39 / A5.39M
Specification for Flux and Electrode Combinations for Submerged Arc and Electroslag Joining and Surfacing of Stainless Steel and Nickel Alloys
Combined standard for SAW flux + electrode matched set for stainless steel and nickel alloy submerged arc welding.
Application: Thick stainless steel and nickel alloy plate SAW welding for chemical and marine equipment.
The AWS A5 series filler metal system covers nearly all mainstream welding consumables for ferrous and non-ferrous metals. Users can select
SMAW stick electrodes, GMAW solid wires, FCAW flux-cored wires, metal-cored wires, SAW wires & fluxes, brazing fillers and cladding powders
according to base material, mechanical requirement, service temperature, corrosion environment and welding process. Correct selection of AWS
classified welding consumables ensures stable weld metal mechanical performance, corrosion resistance and long-term service reliability for critical industrial projects.
AWS A5 series standards define welding electrodes, solid wires, flux cored wires, rods, fluxes and cladding powders for carbon steel, low alloy steel,
stainless steel, aluminium, copper, nickel, titanium, magnesium and cast iron welding, widely used in aerospace, chemical, marine and new energy industries.
How to choose a suitable AWS A5.16 ERTi1 ERTi2 ERTi5 Titanium Solid Welding Wire?
Select the titanium filler metal mainly based on your base material, service load and corrosion environment. Choose ERTi‑1 when welding Ti Grade 1 for applications requiring maximum ductility and corrosion resistance under low load. ERTi‑2 is the preferred general grade for welding Ti Grade1 to Grade4 commercially pure titanium for chemical, heat exchanger and seawater projects. Pick ERTi‑5 (Ti‑6Al‑4V) for joining Ti Grade5 (Ti‑6Al‑4V) alloy where high strength and lightweight structural performance are required. Cross-grade substitution needs formal engineering review.
Short bullet points
Base metal = Ti Grade1, low load, high ductility & corrosion requirement → ERTi‑1
Base metal = Ti Grade1/2/3/4 CP titanium, chemical / seawater / heat exchanger → ERTi‑2
Base metal = Ti‑6Al‑4V Grade5, high strength structural parts → ERTi‑5
Do not swap grades freely; substitution must get engineering approval
All titanium wires require full high-purity argon shielding
 English
 العربية
 Français
 Русский
 Español
 Português
 Deutsch
 italiano
 日本語
 한국어
 Nederlands
 Tiếng Việt
 ไทย
 Polski
 Türkçe
 Bahasa Melayu
 Filipino
 Bahasa Indonesia
 magyar
 Română
 Čeština
 Монгол
 қазақ
 Српски
 हिन्दी
 فارسی
 Slovenčina
 Slovenščina
 Norsk
 Svenska
 українська
 Ελληνικά
 Suomi
 Հայերեն
 עברית
 Dansk
 اردو
 বাংলা
 Hrvatski
 Afrikaans
 Gaeilge
 Eesti keel
 Māori
 नेपाली
 Oʻzbekcha
 latviešu
 Azərbaycan dili
 Беларуская мова
 Български
 Kurdî
 Кыргызча