You are here:Home » News » What is the complete list of AWS A5.9 / A5.9M types?
What is the complete list of AWS A5.9 / A5.9M types?
Views: 0 Author: Site Editor Publish Time: 2026-09-24 Origin: Site
AWS A5.9 / A5.9M is the American Welding Society specification that classifies bare stainless steel welding electrodes and rods for gas-shielded and submerged arc processes. Buyers and welding engineers who work with stainless steel fabrication frequently need the complete classification list to match a filler metal with a base metal grade. This article explains how AWS A5.9 works, lists every classification in the specification, and offers a practical selection framework for procurement teams and workshop operators.
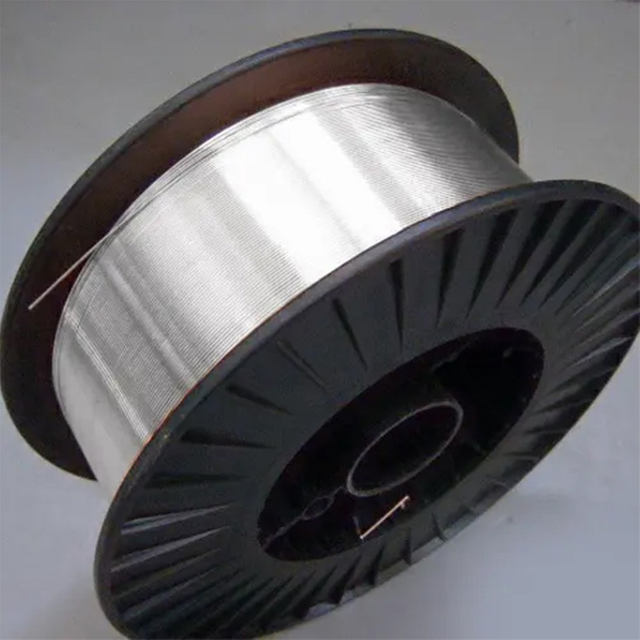
Image Source: Sanzhong Welding (asweld.com)
Key Takeaways
AWS A5.9 covers bare stainless steel filler metals in wire, rod, strip, and metal-cored forms for GMAW, SAW, GTAW, and PAW.
Classifications use the ER prefix plus an alloy number (308, 316, 347, 2209, 2594) and optional letter suffixes such as L, H, Si, Mo, and Nb.
The complete AWS A5.9 list contains approximately 45 classifications grouped into austenitic, martensitic, ferritic, duplex, superduplex, precipitation-hardening, and specialized families.
ER308L and ER316L are the most widely specified austenitic filler metals, with matching chemistry for 304 and 316 base metals.
Duplex and superduplex grades such as ER2209 and ER2594 deliver 100,000 to 116,000 psi minimum tensile strength for demanding chloride service.
Chemical composition and mechanical requirements are defined per classification; values should always be verified against the current edition of AWS A5.9 / A5.9M.
Related standards include AWS A5.4, A5.22, A5.30, and the international equivalent ISO 14343.
Buyers should request a manufacturer datasheet and certificate of conformance when sourcing stainless steel welding wire to AWS A5.9.
What Is AWS A5.9 / A5.9M?
AWS A5.9 / A5.9M is the specification titled "Specification for Bare Stainless Steel Welding Electrodes and Rods." It prescribes the requirements for classification of bare stainless steel electrodes, both as wire and strip, for gas metal arc welding (GMAW), submerged arc welding (SAW), and other fusion welding processes. It also includes wire and rods for use in gas tungsten arc welding (GTAW) and plasma arc welding (PAW). Classification is based on the chemical composition of the filler metal, so the weld deposit meets the required corrosion resistance and mechanical properties. The chromium content of these filler metals is not less than 10.5%, and the iron content exceeds that of any other element.
The current edition is AWS A5.9 / A5.9M:2022, the 10th edition, which revises the 2017 edition. The specification is also adopted as ASME SFA-5.9 and appears in Section II, Part C of the ASME Boiler and Pressure Vessel Code. Always verify specific classification requirements with the latest edition.
What Is the Scope of AWS A5.9 / A5.9M?
AWS A5.9 / A5.9M covers bare stainless steel filler metals for gas-shielded and submerged arc welding processes. The specification applies to solid wires, composite metal-cored electrodes, and strip electrodes used for welding stainless and heat-resisting steels. It addresses filler metals for welding austenitic, martensitic, ferritic, duplex, and precipitation-hardening stainless steels. For covered stainless steel electrodes used with the shielded metal arc welding (SMAW) process, the applicable standard is AWS A5.4 / A5.4M. For flux cored and metal cored stainless steel electrodes, AWS A5.22 / A5.22M is the applicable standard.
How Are AWS A5.9 Filler Metals Classified?
Stainless steel filler metals under this specification are classified using an alphanumeric system that begins with the prefix "ER" for electrode or rod. The prefix is followed by a numerical designation that identifies the nominal chemical composition, such as 308, 316, 347, 2209, or 2594. Letters may follow the numerical designation to indicate specific compositional variants. For example, ER308L indicates a low-carbon 308 filler metal, and ER316LSi indicates a low-carbon 316 filler metal with higher silicon content. The table below summarizes the most common suffix letters.
Suffix
Meaning
Example
L
Low carbon (max 0.03% C)
ER308L, ER316L
H
High carbon (controlled minimum carbon)
ER308H, ER316H
Si
Higher silicon (0.65%–1.00%)
ER308LSi, ER316LSi, ER347Si
Mo
Molybdenum-bearing variant
ER308Mo, ER309Mo, ER410NiMo
Nb
Niobium-stabilized
ER409Nb
What Is the Complete List of AWS A5.9 / A5.9M Types?
The AWS A5.9 / A5.9M classification list comprises approximately 45 bare stainless steel filler metals organized by alloy family. The table below groups every classification by family for quick reference. For the complete and authoritative list in the current edition, always verify with the latest AWS A5.9 / A5.9M specification.
The 200 series classifications contain manganese and nitrogen as partial substitutes for nickel. This composition provides higher strength than the standard 300 series while maintaining good formability and corrosion resistance. ER209, ER219, and ER240 are specified where high manganese austenitic filler metals are required.
300 Series Overview
The 300 series is the largest group in AWS A5.9. It includes workhorse grades such as ER308 and ER308L for 304-type base metals, ER309 and ER309L for dissimilar and overlay welding, ER310 for high-temperature service, ER312 for dissimilar joints and hard surfacing, ER316 and ER316L for molybdenum-bearing corrosion service, ER317 and ER317L for higher pitting resistance, ER320 and ER320LR for corrosion-resistant chemical service, ER330 for elevated-temperature service, and ER347 for stabilized grades. High-alloy grades ER383 and ER385 serve aggressive chemical environments.
ER308L: Properties, Applications, and Shielding Gas
ER308L is a low-carbon austenitic stainless steel bare welding wire and rod designed for welding Type 304L and Type 304 stainless steels. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.03%, chromium at 19.5% to 22.0%, nickel at 9.0% to 11.0%, and molybdenum at a maximum of 0.75%. Manganese is present at 1.0% to 2.5%, and silicon at 0.30% to 0.65%. The filler metal delivers a minimum tensile strength of 75,000 psi (520 MPa) and a minimum elongation of 35%. The low carbon content provides improved resistance to intergranular corrosion by preventing chromium carbide precipitation during welding and elevated-temperature service.
ER308L is the most widely used stainless steel filler metal for general fabrication of 304 and 304L stainless steels in food and beverage equipment, chemical processing, and petrochemical applications. It is also suitable for welding dissimilar 300 series stainless steels where matching or near-matching chemistry is required. Typical applications include tanks, piping, vessels, and structural components made from 304 stainless steel. ER308L is available in solid wire form for GMAW and SAW, and in straight rod form for GTAW.
ER308L is typically welded with a mixture of 98% argon and 2% oxygen (or 98% argon and 2% CO₂) for GMAW applications. For GTAW, 100% argon is commonly used. For SAW, a suitable stainless steel flux is required along with the filler metal. The choice of shielding gas affects arc stability, bead appearance, and the oxygen content of the weld metal, which in turn influences corrosion resistance and mechanical properties.
ER316L: Properties, Applications, and the ER316L vs ER316LSi Difference
ER316L is a low-carbon molybdenum-bearing austenitic stainless steel bare welding wire and rod designed for welding Type 316L and Type 316 stainless steels. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.03%, chromium at 18.0% to 20.0%, nickel at 11.0% to 14.0%, and molybdenum at 2.0% to 3.0%. Manganese is present at 1.0% to 2.5%, and silicon at 0.30% to 0.65%. The filler metal delivers a minimum tensile strength of 75,000 psi (520 MPa) and a minimum elongation of 35%. The molybdenum addition provides improved resistance to pitting and crevice corrosion in chloride-containing environments, as well as increased creep resistance at elevated temperatures. The low carbon content prevents sensitization and intergranular corrosion during welding and high-temperature service.
ER316L is used for welding Type 316 and Type 316L stainless steels in chemical processing equipment, petrochemical plants, and marine environments. It is also used for welding components exposed to chlorides where pitting resistance is important. Typical applications include piping, tanks, heat exchangers, and valves made from 316 stainless steel. ER316L is particularly suitable for applications involving acetic acid, sulfuric acid, and other corrosive chemicals where molybdenum-bearing stainless steels are required.
ER316L and ER316LSi differ primarily in their silicon content and resulting welding characteristics. ER316L contains silicon at 0.30% to 0.65%, while ER316LSi contains silicon at 0.65% to 1.00%. The higher silicon content in ER316LSi improves weld pool fluidity, wetting, and bead appearance, making it particularly suitable for GMAW and for welding in the flat and horizontal positions. However, higher silicon content may reduce corrosion resistance in some environments due to the formation of silicon-rich phases. ER316L is generally preferred for GTAW and for applications requiring maximum corrosion resistance, while ER316LSi is preferred for GMAW and for applications where weld appearance and productivity are priorities.
ER347: Properties, Applications, and the ER347 vs ER347Si Difference
ER347 is a niobium-stabilized austenitic stainless steel bare welding wire and rod designed for welding Type 321 and Type 347 stainless steels, as well as for high-temperature service. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.08%, chromium at 19.0% to 21.5%, nickel at 9.0% to 11.0%, and niobium plus tantalum at a minimum of 10 times the carbon content to a maximum of 1.00%. Manganese is present at 1.0% to 2.5%, and silicon at 0.30% to 0.65%. The niobium addition stabilizes the deposit against sensitization by forming niobium carbides instead of chromium carbides, preventing intergranular corrosion in high-temperature service. ER347 delivers a minimum tensile strength of 75,000 psi (520 MPa) and a minimum elongation of 30%.
ER347 is used for welding Type 321 and Type 347 stainless steels in high-temperature service, such as furnace components, heat exchangers, and piping in petrochemical plants. It is also used for welding stabilized stainless steels where resistance to intergranular corrosion is critical. Typical applications include high-temperature process equipment, exhaust systems, and components exposed to thermal cycling. ER347 is particularly suitable for components that cannot be post-weld heat treated and must resist sensitization during elevated-temperature exposure.
ER347 and ER347Si differ primarily in their silicon content and resulting welding characteristics. ER347 contains silicon at 0.30% to 0.65%, while ER347Si contains silicon at 0.65% to 1.00%. The higher silicon content in ER347Si improves weld pool fluidity and bead appearance, similar to the difference between ER316L and ER316LSi. ER347Si is often preferred for GMAW applications where smooth bead appearance and good wetting are important, while ER347 is preferred for GTAW and applications requiring maximum corrosion resistance.
Martensitic and Ferritic Classifications
The martensitic and ferritic classifications include ER409Nb, ER410, ER410NiMo, ER420, ER430, ER439, ER446, and ER446LMo. ER409Nb is a niobium-stabilized ferritic filler metal for exhaust system components. ER410 and ER410NiMo are 13% chromium martensitic filler metals for turbine and valve applications where wear resistance and moderate corrosion resistance are required. ER420 is a martensitic filler metal for hard surfacing and tooling applications. ER430 and ER439 are 17% chromium ferritic filler metals with good oxidation resistance. ER446 and ER446LMo are high-chromium ferritic filler metals for elevated-temperature service. These classifications cover the 400 series base metal family and are selected when matching or near-matching chemistry is required.
Duplex and Superduplex Classifications
ER2209: Properties, Applications, and Shielding Gas
ER2209 is a duplex stainless steel bare welding wire and rod designed for welding 22% chromium duplex stainless steels such as UNS S31803 and S32205. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.03%, chromium at 22.0% to 24.0%, nickel at 8.5% to 10.5%, molybdenum at 2.5% to 3.5%, and nitrogen at 0.10% to 0.20%. The duplex microstructure provides high strength combined with excellent resistance to stress corrosion cracking and pitting corrosion. ER2209 typically delivers a minimum tensile strength of 100,000 psi (690 MPa) or higher, significantly exceeding that of austenitic stainless steel filler metals.
ER2209 is used for welding duplex stainless steel components in offshore oil and gas platforms, chemical tankers, desalination plants, and pulp and paper processing equipment. It is particularly suitable for applications requiring high strength combined with resistance to chloride stress corrosion cracking. Typical applications include piping, pressure vessels, heat exchangers, and structural components made from 2205 duplex stainless steel. ER2209 is available in solid wire form for GMAW and SAW, and in straight rod form for GTAW.
ER2209 is typically welded with a mixture of 98% argon and 2% oxygen or 98% argon and 2% CO₂ for GMAW applications. For GTAW, 100% argon is commonly used. Nitrogen additions to the shielding gas (typically 1% to 2%) may be used to promote austenite formation in the weld metal and improve corrosion resistance. The choice of shielding gas affects the ferrite-austenite balance in the weld deposit, which in turn influences mechanical properties and corrosion resistance.
ER2594: Properties and Applications
ER2594 is a superduplex stainless steel bare welding wire and rod designed for welding superduplex stainless steels such as UNS S32750 and S32760. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.03%, chromium at 24.0% to 27.0%, nickel at 8.0% to 10.5%, molybdenum at 2.5% to 4.5%, and nitrogen at 0.20% to 0.30%. The higher alloy content provides superior resistance to pitting and crevice corrosion compared with standard duplex filler metals, with a pitting resistance equivalent number (PREN) exceeding 40. ER2594 delivers high tensile strength of approximately 116,000 psi (800 MPa) minimum and excellent toughness, making it suitable for the most demanding corrosive environments.
ER2594 is used for welding superduplex stainless steel components in offshore platforms, subsea equipment, seawater piping, and chemical processing plants. It is particularly suitable for applications requiring maximum resistance to chloride pitting and stress corrosion cracking. Typical applications include manifolds, risers, pumps, valves, and heat exchangers made from superduplex stainless steels such as 2507. ER2594 is also used for welding duplex stainless steels when higher corrosion resistance is required than ER2209 can provide.
ER2553 vs ER2594
ER2553 and ER2594 are both superduplex filler metals, but they differ in their alloy composition and intended base metals. ER2553 contains copper (approximately 2%) and has lower nickel content (approximately 5.5%), making it suitable for welding 25% chromium duplex stainless steels with copper additions. ER2594 contains no deliberate copper addition and has higher nickel content (approximately 9%), making it suitable for welding 25% chromium superduplex stainless steels without copper. Both classifications provide high strength and excellent corrosion resistance; the choice between them depends on the specific base metal composition and the required corrosion performance.
Precipitation-Hardening and Specialized Classifications
ER630: Properties, Applications, and Heat Treatment
ER630 is a precipitation-hardening stainless steel bare welding wire and rod designed for welding ASTM A564 Type 630 (17-4 PH) and similar precipitation-hardening stainless steels. Its typical deposited weld metal chemistry includes carbon at a maximum of 0.05%, chromium at 16.0% to 16.75%, nickel at 4.5% to 5.0%, copper at 3.25% to 4.00%, and niobium at 0.15% to 0.30%. The filler metal delivers high strength through precipitation hardening heat treatment, with tensile strength typically in the range of 130,000 to 190,000 psi depending on the heat treatment condition.
ER630 is used for welding 17-4 PH components in aerospace, petrochemical, and nuclear applications. Typical applications include turbine blades, valve components, pump shafts, and structural components requiring high strength and moderate corrosion resistance. The filler metal is suitable for both solution-annealed and aged conditions, and post-weld heat treatment may be required to achieve the desired mechanical properties. Post-weld heat treatment for ER630 typically involves solution annealing at approximately 1040°C (1900°F) followed by rapid cooling, then aging at approximately 480°C to 620°C (900°F to 1150°F) for 1 to 4 hours depending on the desired strength and toughness combination. The exact heat treatment parameters should be verified with the manufacturer's datasheet and the applicable material specification.
ER16-8-2 and ER18SR
ER16-8-2 is a hybrid alloy between 308H and 316H designed for high-temperature applications, with a nominal composition of approximately 15.5% Cr, 8.5% Ni, and 1.2% Mo. ER18SR is a specialized filler metal for high-temperature service, with a nominal composition designed for applications where resistance to scaling and creep is required. These classifications address specific application requirements that are not met by the standard austenitic or ferritic grades.
Chemical Composition Requirements in AWS A5.9
AWS A5.9 specifies chemical composition requirements for each classification of bare stainless steel filler metal. The composition requirements control carbon, chromium, nickel, molybdenum, manganese, silicon, phosphorus, sulfur, nitrogen, copper, niobium, titanium, and other elements within specified maximum or range limits. These requirements ensure that the weld deposit achieves the intended corrosion resistance, mechanical properties, and microstructural characteristics. The table below summarizes the typical ranges for the most widely specified grades; the exact limits for every classification are provided in the standard and should be verified with the latest edition.
Classification
Carbon
Chromium
Nickel
Molybdenum
ER308L
0.03 max
19.5–22.0
9.0–11.0
0.75 max
ER316L
0.03 max
18.0–20.0
11.0–14.0
2.0–3.0
ER347
0.08 max
19.0–21.5
9.0–11.0
0.75 max
ER2209
0.03 max
22.0–24.0
8.5–10.5
2.5–3.5
ER2594
0.03 max
24.0–27.0
8.0–10.5
2.5–4.5
ER630
0.05 max
16.0–16.75
4.5–5.0
0.75 max
Carbon content varies by classification: low-carbon (L) grades such as ER308L and ER316L are limited to a maximum of 0.03%, standard grades such as ER308 and ER316 to a maximum of 0.08%, and high-carbon (H) grades such as ER308H have controlled minimum carbon levels for elevated-temperature strength. Chromium content ranges from approximately 18.0% to 27.0% across the classification list and is always maintained above 10.5% to ensure stainless properties. Higher chromium grades provide improved resistance to oxidation and high-temperature corrosion. Nickel content varies from approximately 8.0% to 14.0%, and molybdenum from 2.0% to 4.5% in molybdenum-bearing grades, providing improved pitting and crevice corrosion resistance. The nickel-to-chromium ratio is carefully controlled to ensure the correct balance of austenite and ferrite in the weld deposit.
Mechanical Properties of AWS A5.9 Filler Metals
The mechanical properties of AWS A5.9 filler metals are determined through tensile tests of the all-weld metal. Tensile strength requirements vary by classification, reflecting the different alloy systems and their intended applications. Elongation requirements ensure adequate ductility for the intended service conditions. For duplex and superduplex classifications, impact toughness requirements are also specified, typically at temperatures ranging from −20°C to −50°C. The table below summarizes the minimum tensile strength for the main alloy families; exact values for each classification should be verified with the latest edition.
Alloy Family
Representative Grades
Minimum Tensile Strength
Austenitic (300 series)
ER308L, ER316L, ER347
75,000 psi (520 MPa)
Austenitic (200 series)
ER209, ER240
100,000 psi (690 MPa)
Austenitic (high-alloy)
ER383, ER385
75,000–85,000 psi (520–590 MPa)
Duplex
ER2209
100,000 psi (690 MPa)
Superduplex
ER2553 / ER2594
110,000–116,000 psi (760–800 MPa)
Precipitation-hardening
ER630
130,000–190,000 psi (depending on heat treatment)
How to Choose the Right AWS A5.9 Filler Metal
Selecting the right filler metal depends on the base metal composition, the required corrosion resistance, the mechanical properties, the service temperature, and the welding process. The decision framework below walks through five practical steps.
Step 1 — Identify the base metal family. Select the matching filler metal family: 200 series for high-manganese austenitic, 300 series for standard austenitic, 400 series for martensitic and ferritic, and 2209/2553/2594 for duplex and superduplex base metals.
Step 2 — Determine the carbon level. Choose an "L" grade for maximum corrosion resistance and resistance to sensitization, a standard grade for general purpose, or an "H" grade for elevated-temperature strength.
Step 3 — Select the product form for the process. Solid wire for GMAW and SAW, straight rod for GTAW, and composite metal-cored wire for GMAW and SAW.
Step 4 — Verify the mechanical property requirements. This matters most for duplex and superduplex filler metals, where high strength and impact toughness are key requirements.
Step 5 — Confirm code and specification compliance. Check applicable code requirements such as ASME Section IX F-Number and A-Number designations. Most stainless steel filler metals in the standard are grouped under F-Number 6, which covers austenitic and duplex stainless steels, including ER308L, ER316L, ER347, and ER2209. The A-Number groups filler metals by the chemical composition of the deposited weld metal, with distinct designations for austenitic, duplex, and superduplex alloy types. The exact F-Number and A-Number assignments should be verified with the latest edition of ASME Section IX.
Base Metal
Recommended AWS A5.9 Filler Metal
Type 304 / 304L
ER308 / ER308L
Type 316 / 316L
ER316 / ER316L (ER316LSi for GMAW)
Type 321 / 347
ER347
2205 duplex (UNS S31803 / S32205)
ER2209
2507 superduplex (UNS S32750 / S32760)
ER2594
17-4 PH (ASTM A564 Type 630)
ER630
Related Standards to Know
AWS A5.9 is part of a broader family of AWS filler metal specifications for stainless steel and other materials. Understanding these related standards helps ensure that the correct specification is applied for each welding process and base metal.
AWS A5.4 / A5.4M covers stainless steel covered electrodes for shielded metal arc welding. It includes classifications such as E308L-16, E316L-17, E347-16, and E2209-15, which correspond to many of the bare filler metal classifications in AWS A5.9. These covered electrodes are used for manual stick welding of stainless steels, while AWS A5.9 bare wires and rods are used for gas-shielded and submerged arc processes.
AWS A5.22 / A5.22M covers stainless steel flux cored and metal cored electrodes and rods for arc welding. It includes classifications such as E308LT1-1, E316LT1-1, and E2209T1-1, used with flux cored arc welding (FCAW) and metal cored arc welding processes. New classifications in the 2024 edition also include the metal cored electrodes currently listed in AWS A5.9 / A5.9M; in the next revision of AWS A5.9 / A5.9M, these metal cored electrodes will be deleted from that specification.
AWS A5.30 / A5.30M covers consumable inserts used in root pass welding of pipe and tube, including stainless steel, nickel alloy, and carbon steel inserts used with gas tungsten arc welding.
ISO 14343 is the international standard for wire electrodes, strip electrodes, wires, and rods for arc welding of stainless and heat-resisting steels, published by the International Organization for Standardization (ISO 14343:2025). The ISO 14343 classification system uses a different designation structure than AWS A5.9, but many products carry dual classifications under both systems. For example, ER308L under AWS A5.9 corresponds to ISO 14343-A G 19 9 L or W 19 9 L, and ER316L corresponds to ISO 14343-A G 19 12 3 L or W 19 12 3 L. The correspondence is product-specific and should be verified with the manufacturer's datasheet and the latest editions of both standards.
Where to Find the Official Complete List of AWS A5.9 / A5.9M Types
The authoritative source for the complete list of AWS A5.9 / A5.9M classifications is the latest edition of the specification itself, available from the American Welding Society at pubs.aws.org or through authorized standards distributors. The specification includes detailed tables covering chemical composition requirements, mechanical property minimums, product forms, and packaging requirements for every classification. Manufacturer technical datasheets and welding consumable catalogs also list AWS A5.9 classifications, but these should be cross-referenced against the official specification for accuracy. Because classifications may be added or revised with each edition, always verify with the latest AWS A5.9 / A5.9M edition to ensure your filler metal selection aligns with the current classification list.
Summary
The specification organizes bare stainless steel welding electrodes and rods into approximately 45 classifications across austenitic, martensitic, ferritic, duplex, superduplex, precipitation-hardening, and specialized families. The ER prefix plus alloy number and suffix letters quickly identify the chemistry and intended service. ER308L, ER316L, and ER347 cover the most common austenitic applications; ER2209 and ER2594 serve high-strength duplex service; and ER630 covers precipitation-hardening base metals. Chemical composition and mechanical requirements are defined per classification, and every value should be checked against the current edition of the specification before purchase. Buyers sourcing stainless steel welding wire should request a datasheet, a mill certificate of conformance, and confirmation that the product is classified to AWS A5.9 / A5.9M.
Need AWS A5.9 Stainless Steel Welding Wire?
SANZHONG WELDING is a welding wire manufacturer in Changzhou, China, supplying stainless steel MIG welding wire, TIG rod, and SAW wire classified to AWS A5.9 / A5.9M, with grades such as ER308L, ER316L, ER316LSi, ER347, ER2209, and ER2594. Buyers can request a quotation, a composition certificate, or spool/coil specifications before ordering.
AWS A5.9 / A5.9M classifies bare stainless steel welding electrodes and rods for GMAW, SAW, GTAW, and PAW, covering solid wire, composite metal-cored wire, and strip in austenitic, martensitic, ferritic, duplex, superduplex, and precipitation-hardening grades.
What is the difference between AWS A5.9 and AWS A5.4?
AWS A5.9 covers bare (uncoated) stainless steel wire and rods for gas-shielded and submerged arc processes. AWS A5.4 covers covered electrodes for shielded metal arc welding (stick welding). They cover different product forms and processes.
What does ER308L mean?
ER means electrode or rod, 308 identifies the 308 alloy family, and L indicates low carbon (0.03% max). ER308L is the standard filler metal for welding 304 and 304L stainless steel.
How many classifications are in AWS A5.9?
The AWS A5.9 list contains approximately 45 classifications, including 200 and 300 series austenitic grades, 400 series martensitic and ferritic grades, duplex and superduplex grades, ER630, and specialized grades.
What is the difference between ER308L and ER308?
ER308L limits carbon to 0.03% maximum, which prevents chromium carbide precipitation and improves resistance to intergranular corrosion. ER308 allows up to 0.08% carbon and is used for general applications where sensitization is not a concern.
Which AWS A5.9 filler metal is used for 304 and 316 stainless steel?
ER308 or ER308L for 304/304L, and ER316 or ER316L for 316/316L. For GMAW with appearance priorities, ER316LSi is a common choice.
What is the difference between AWS A5.9 and ISO 14343?
Both classify stainless steel filler metals, but they use different designation systems. Many products carry dual classifications, for example ER308L corresponds to ISO 14343-A G 19 9 L. Verify the correspondence on the manufacturer's datasheet.
Where can buyers source AWS A5.9 stainless steel welding wire?
Buyers can purchase from welding wire manufacturers and distributors that supply classified products with a datasheet and certificate of conformance. SANZHONG WELDING supplies stainless steel MIG wire, TIG rod, and SAW wire to AWS A5.9 / A5.9M grades.
References and Image Credits
AWS A5.9 / A5.9M:2022, Specification for Bare Stainless Steel Welding Electrodes and Rods — American Welding Society: https://pubs.aws.org/p/2144/a59a59m2022-specification-for-bare-stainless-steel-welding-electrodes-and-rods
ISO 14343:2025, Welding consumables — Wire electrodes, strip electrodes, wires and rods for arc welding of stainless and heat resisting steels — Classification — International Organization for Standardization: https://www.iso.org/standard/86735.html
Note: composition and mechanical values shown above are typical minimums/ranges for the listed grades as commonly published; the exact limits for each classification are defined in the current AWS A5.9 / A5.9M edition and must be verified against the standard and the manufacturer's datasheet before purchase. Mechanical values of ER630 depend on heat treatment condition.